Arc transfer modes change the process window
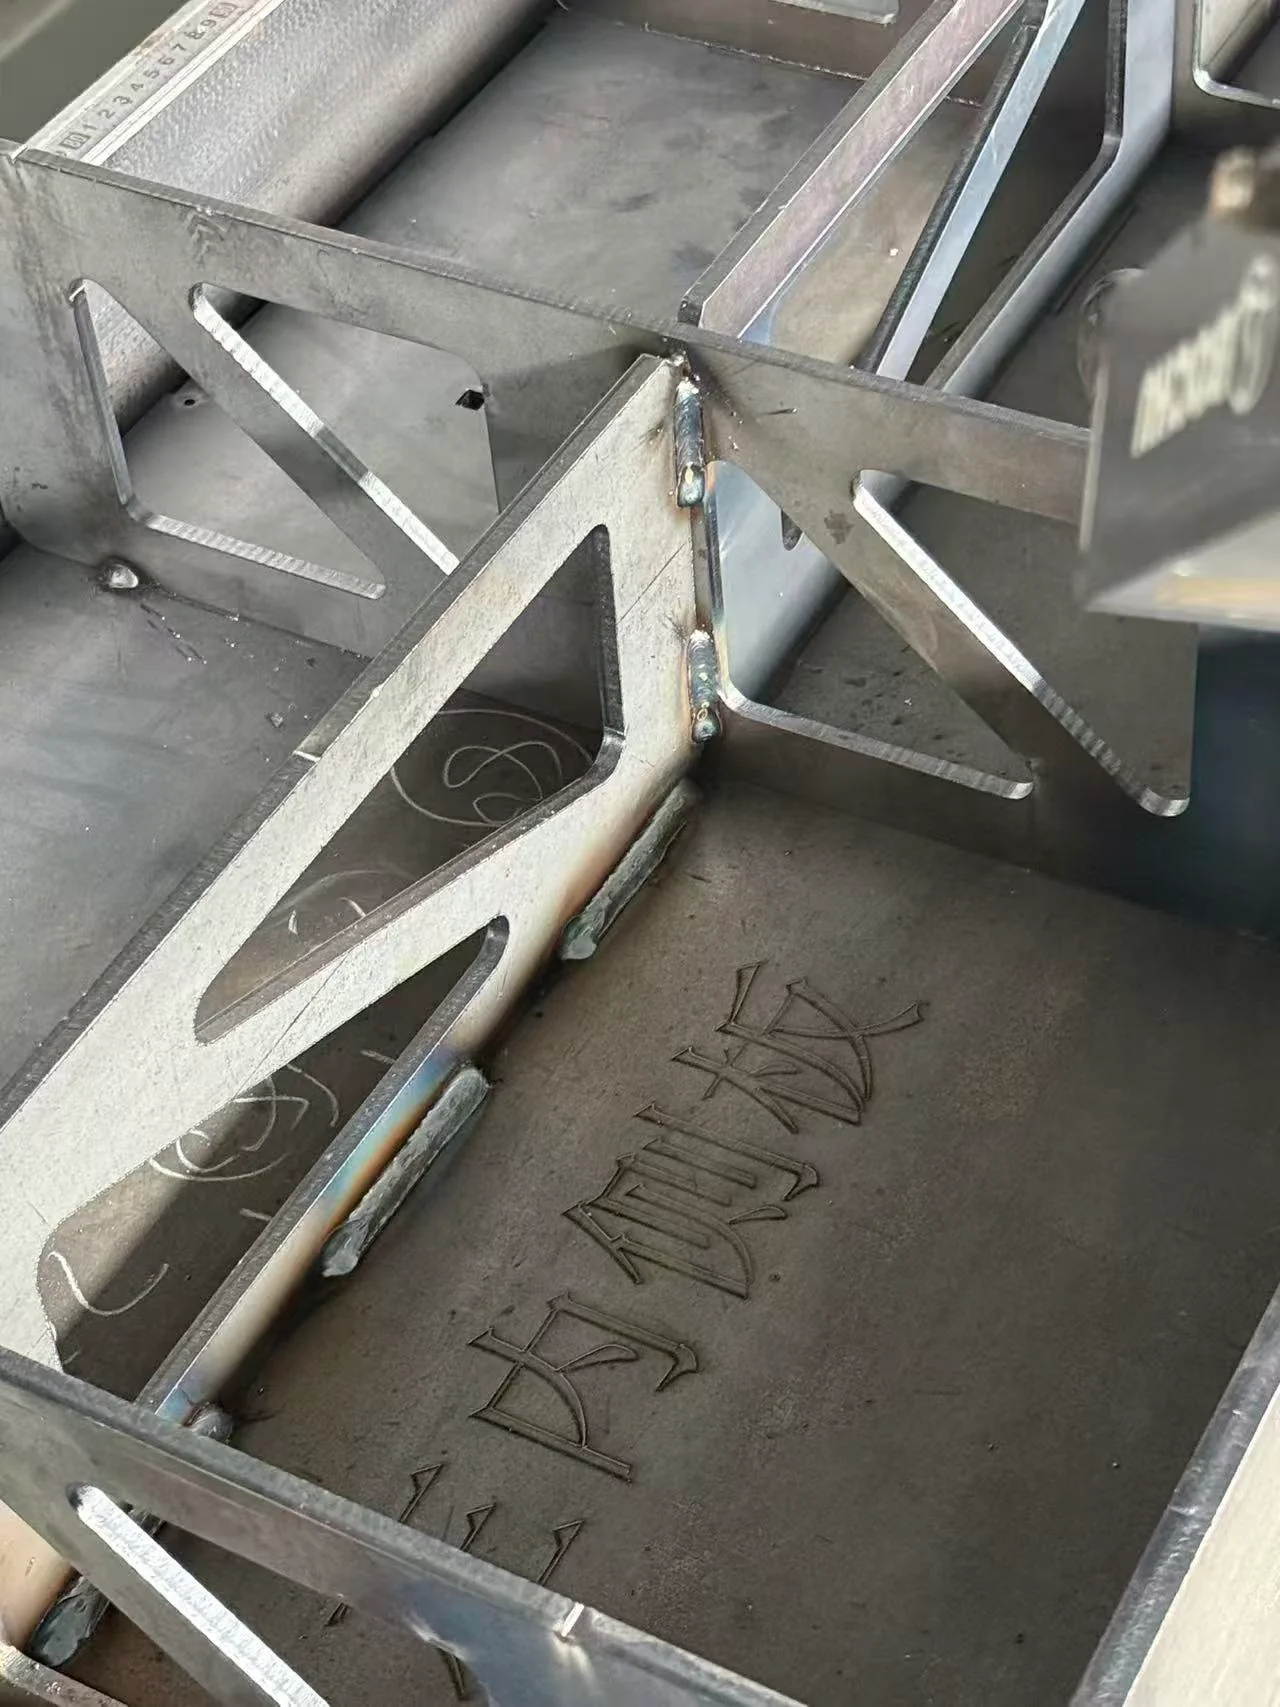
In short-circuit transfer, the wire repeatedly contacts the weld pool as metal transfers. It can serve lower-energy and thin-material tasks, but fusion and spatter still depend on the selected process. Spray transfer uses higher-current conditions and produces a more fluid pool, which affects the suitable joint orientation. Pulsed transfer alternates current levels to control droplet transfer; it requires a compatible source and the appropriate wire/gas program.
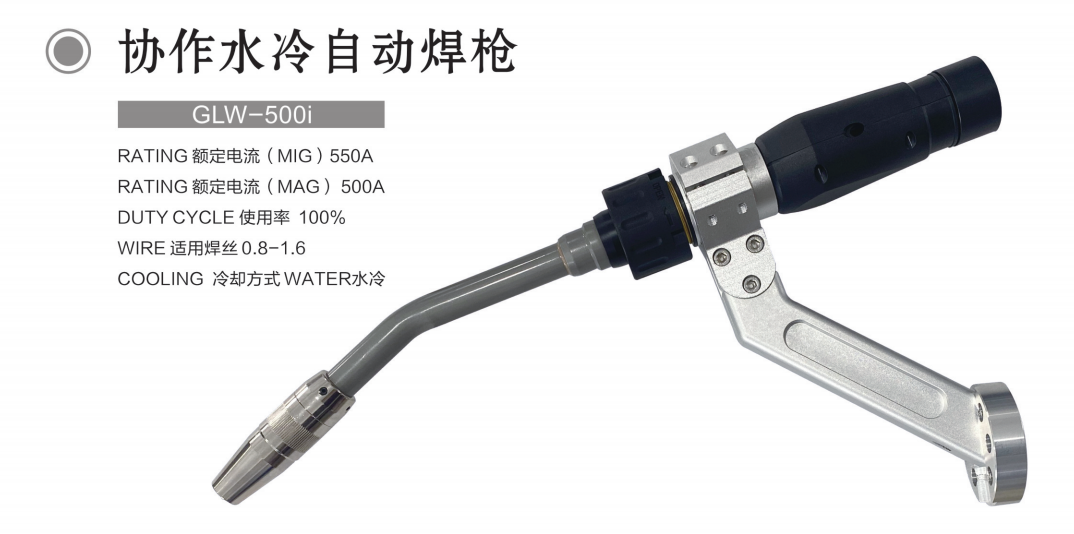
These are process families, not a list of functions included with every CHENDA configuration. The practical comparison is the result on the intended joint: acceptable fusion, bead shape, spatter and heat, at a travel speed the cell can sustain.