Jump to a section
- How Torsion Bar Synchronization Works
- How Y1/Y2 Electro-Hydraulic Control Works
- Why Long Machines Change the Decision
- Which Machine Is More Accurate?
- Off-Center Bending and Short Parts
- Crowning and Backgauge
- Speed, Changeover and Operator Skill
- Cost and Maintenance
- Which Machine Fits Your Work?
- CHENDA Electro-Hydraulic Press Brake Models
- How to Test Both Machines
- Frequently Asked Questions
- Request a Press Brake Recommendation
Quick answer: Torsion bar and electro-hydraulic press brakes both use hydraulic cylinders to create bending force. The main difference is how they keep the two sides of the ram level.
- Start with a torsion bar press brake for repeated, simple bends, a smaller budget and mostly centered work.
- Start with an electro-hydraulic CNC press brake for mixed batches, long machines, off-center work and frequent program changes.
- Check the ram system on the quotation. A CNC screen does not tell you which synchronization system the machine uses.
| Factor | Torsion bar press brake | Electro-hydraulic CNC press brake |
|---|---|---|
| Names buyers may see | NC, torsion axis or torsion shaft press brake | Y1/Y2 CNC or electro-hydraulic synchronized press brake |
| Ram synchronization | Mechanical shaft links both sides | Each side is controlled using position feedback |
| Side-to-side correction | No independent correction from the shaft | Y1 and Y2 can be corrected separately |
| Off-center work | More limited; follow the rated loading instructions | Better suited, but load limits still apply |
| Backgauge | Often fewer CNC axes; confirm the quotation | Often more programmable axes; confirm the quotation |
| Crowning | Manual, controlled or optional, by configuration | Often CNC-adjusted, by configuration |
| Best batch pattern | Stable, repeated parts | Mixed parts and frequent changeovers |
| Maintenance focus | Shaft linkage, alignment and hydraulics | Valves, feedback, controller and hydraulics |
| Purchase price | Usually lower | Usually higher |
Not sure which setup fits your parts? Send CHENDA your part drawing, material and longest bend. Request a Press Brake Recommendation · Email info@chendalaser.com · Phone +86 153 0644 7102
How Torsion Bar Synchronization Works
On a torsion bar press brake, a steel shaft connects the two sides of the ram. Hydraulic cylinders supply the force, while the shaft forces both sides to travel together.
This simple layout has no electronic loop that compares the left and right sides and corrects them during bending. It works best when the setup stays stable and the load stays within the machine’s permitted pattern.
You may see this type described as an NC press brake. Labels are not always consistent, and a torsion bar machine can also have a CNC-style controller. Ask how the ram is synchronized, rather than relying on "NC" or "CNC" alone.
How Y1/Y2 Electro-Hydraulic Control Works
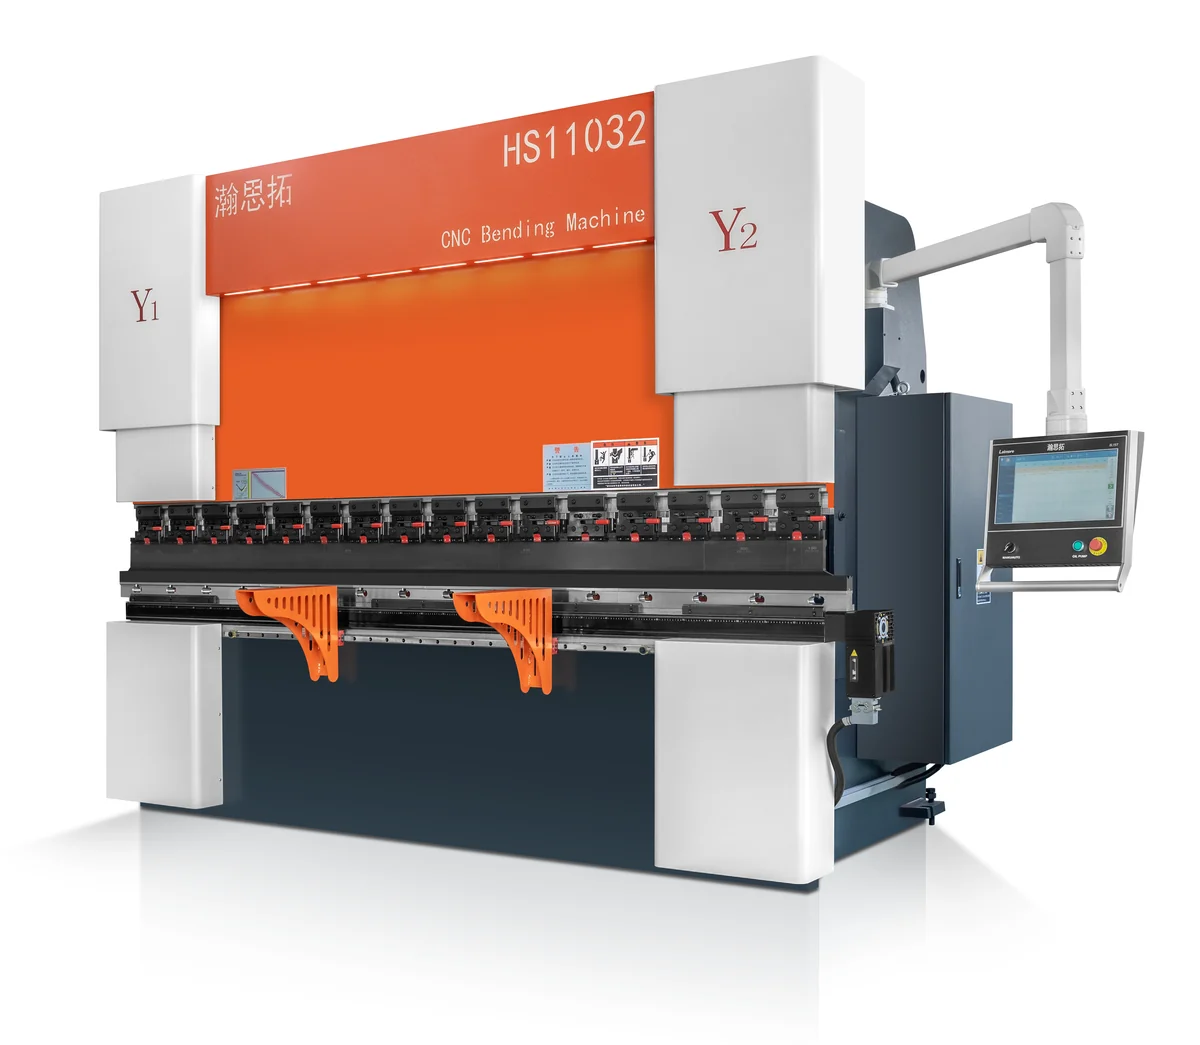
An electro-hydraulic synchronized press brake has no torsion shaft linking the ram sides. The controller uses position feedback to manage the left side (Y1) and right side (Y2).
This gives the operator a separate correction for each end of the bend. It also lets the machine store different positions and sequences for different parts.
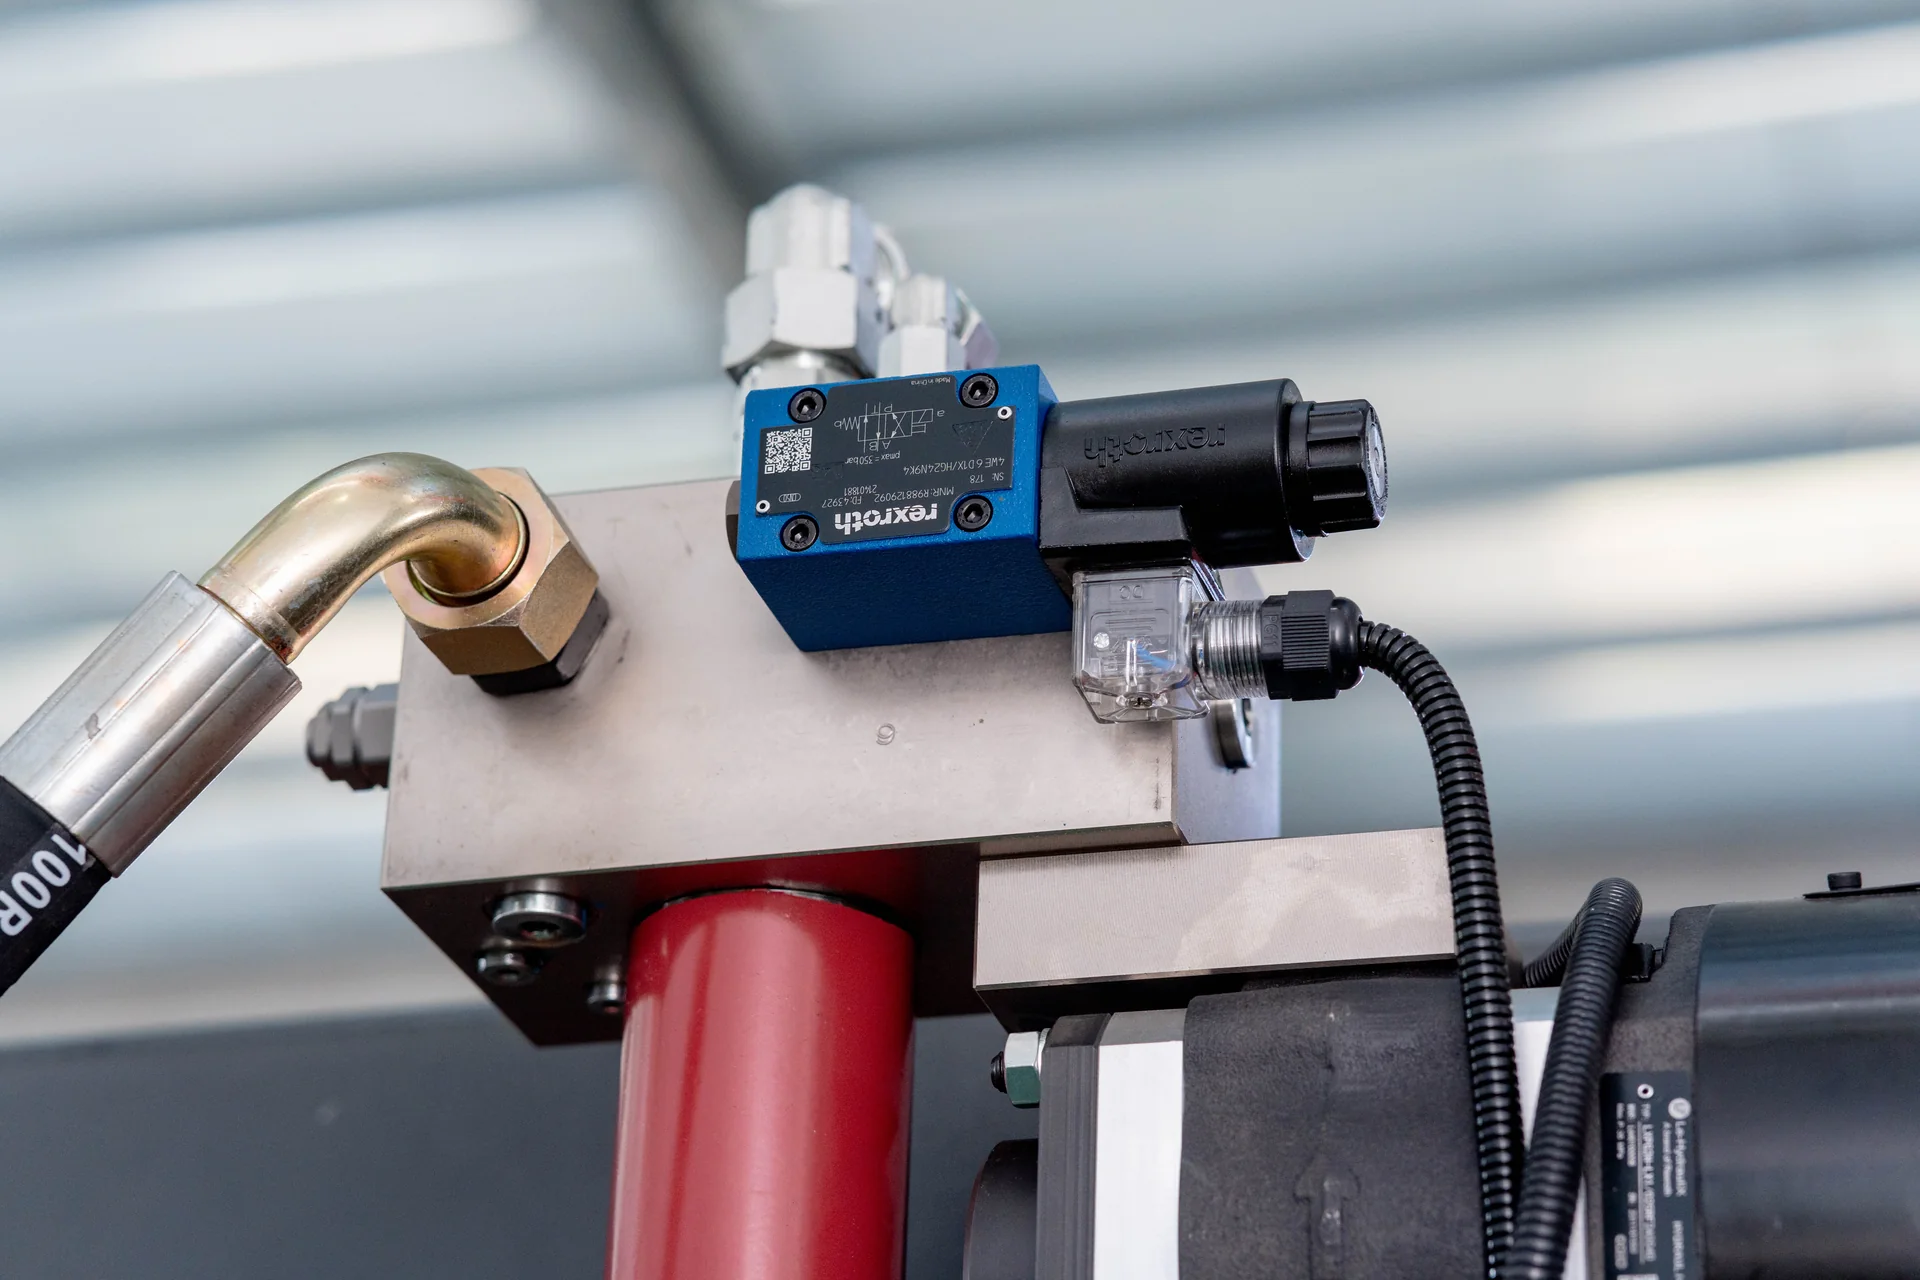
The feedback watches the ram, not the finished bend. If a new material batch springs back more, the ram can reach its target and the angle can still be wrong. Direct angle checking requires a separate measuring system.
Why Long Machines Change the Decision
For the same shaft section, twist increases with length. A longer torsion bar machine therefore depends more on shaft size, frame stiffness and careful loading.
An electro-hydraulic machine can correct the two ram ends separately, which is a key advantage when a long bend shows a side-to-side difference. It does not remove all long-bend problems. Deflection through the middle is a separate issue for crowning.
Crowning alone is therefore not the reason to choose electro-hydraulic control. Either machine type may offer it, so compare the adjustment method and the measured result along the bend.
Which Machine Is More Accurate?
Electro-hydraulic control gives you more ways to correct the process, but neither label guarantees a better finished part. Tooling, material, crowning and setup can decide the result.
The table below shows how the available corrections differ:
| Problem on the part | Torsion bar machine | Electro-hydraulic machine |
|---|---|---|
| One end is more open | Check tools and material, then use the machine’s level adjustment if provided | Check tools and material, then correct Y1 or Y2 |
| Center differs from both ends | Use crowning if fitted | Use crowning if fitted; settings may be CNC-controlled |
| Angle changes with a new batch | Correct depth after a first-part check | Correct and store the program; add angle measurement if fitted |
| Flange length changes | Check the backgauge, part support and bend order | Check the same items; programmed axes may simplify repositioning |
Ask what a stated accuracy figure measures. Ram repeatability is not the same as the tolerance of a finished bend angle.
For any machine you are considering, ask for the ram accuracy figure and a measured sample of your own part before you decide.
The figures below are general published references, not CHENDA specifications or guarantees:
| Item | Published figure | How to read it |
|---|---|---|
| Electro-hydraulic ram positioning | About ±0.01 mm | Machine motion, not the finished angle |
| Torsion bar ram positioning | Often quoted at about ±0.1 mm | Supplier comparison; confirm for the exact machine |
| Finished angle, one supplier comparison | NC: ±0.5°; CNC: about ±0.3° | Depends on tooling, material and process |
| Common target for standard parts | ±0.5° to ±1° | ±0.25° generally needs tighter process control |
Material can matter as much as the machine. In one trade-press example, a ±0.15 mm thickness variation in about 3.3-3.6 mm steel could represent up to 4° of angular variation.
Off-Center Bending and Short Parts
Both machines have loading limits. An off-center bend loads the machine unevenly, and a torsion bar machine is usually more limited in this work. Follow the rated instructions for the exact model.
A short bend can also concentrate the load. Even when the total force is below the machine rating, too much force over a short length can damage tools or permanently deform the ram.
For example, 800 kN/m over a 150 mm engaged length equals 120 kN. This is only an arithmetic example, not a CHENDA tool rating.
To estimate bending force, use the press brake tonnage method and table in our electric vs hydraulic guide.
Crowning and Backgauge
These two systems are not tied to the machine name. Compare the exact package on each quotation.
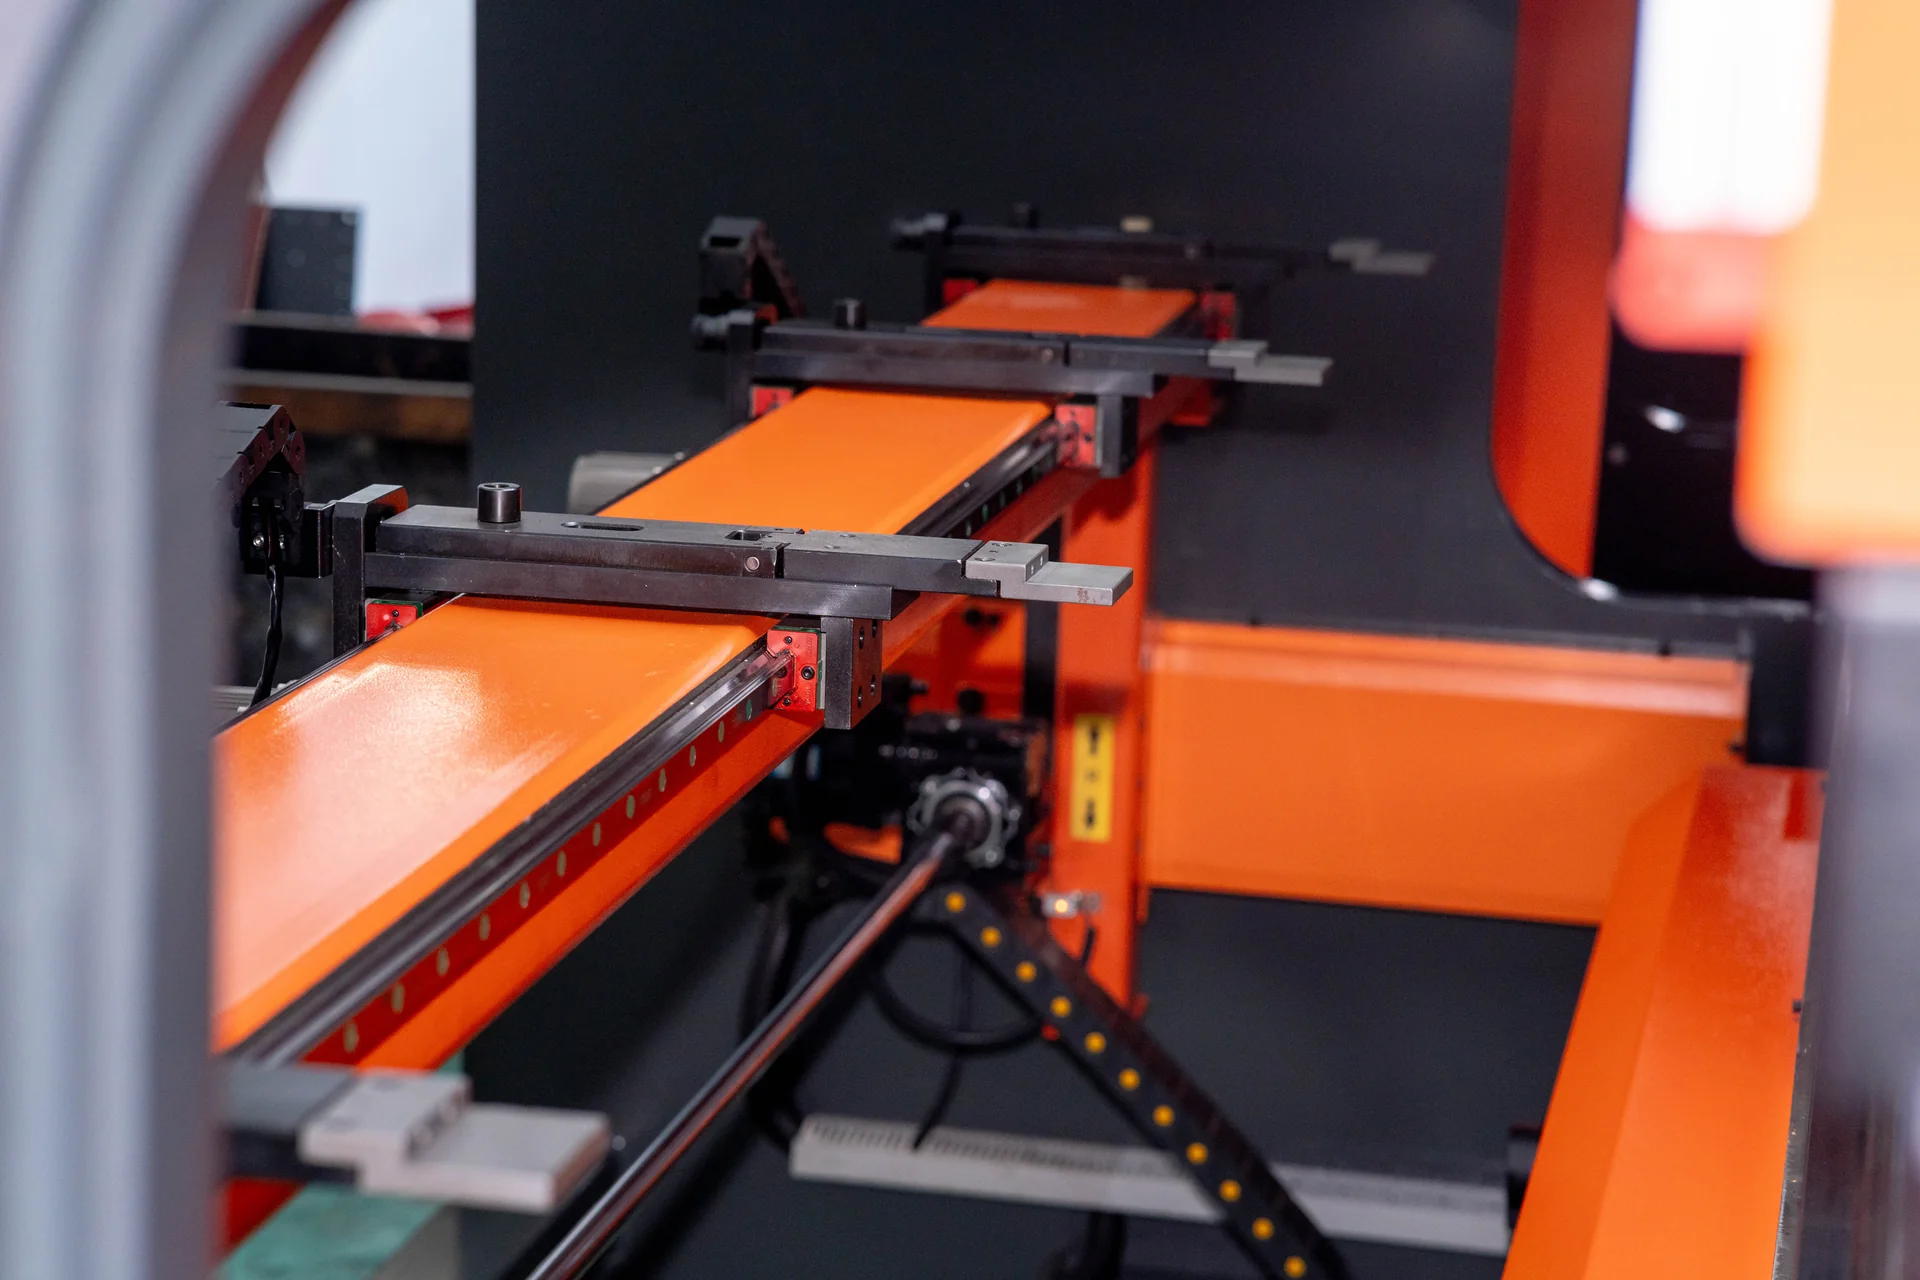
Axis names can also confuse the comparison. X sets gauge depth, R sets finger height, and Z1 and Z2 move the fingers along the bending line. A "6+1" package may count Y1, Y2, X, R, Z1 and Z2, plus crowning.
| Item to compare | Torsion bar machine | Electro-hydraulic machine |
|---|---|---|
| Crowning method | May be manual, controlled or optional | Often adjusted through the CNC |
| Backgauge axes | Often a smaller axis package | Often X and R, with Z1 and Z2 available |
| Finger movement | Check what is manual | Check what is programmed |
| Job recall | Check what the controller stores | Check program, tool and sequence functions |
Speed, Changeover and Operator Skill
Suppliers often describe electro-hydraulic machines as faster, but a general claim cannot estimate your output. Compare approach, bending and return speeds for the exact models, then time the complete job.
As a general reference, published synchronized CNC specifications commonly list about 90-200 mm/s approach, 7-10 mm/s bending and 60-170 mm/s return, with larger machines often slower. One supplier comparison quotes 80-100 mm/s down speed for NC machines and 160-200 mm/s for CNC machines. Faster approach and return can save time, but bending speed stays much lower. These are not CHENDA figures.
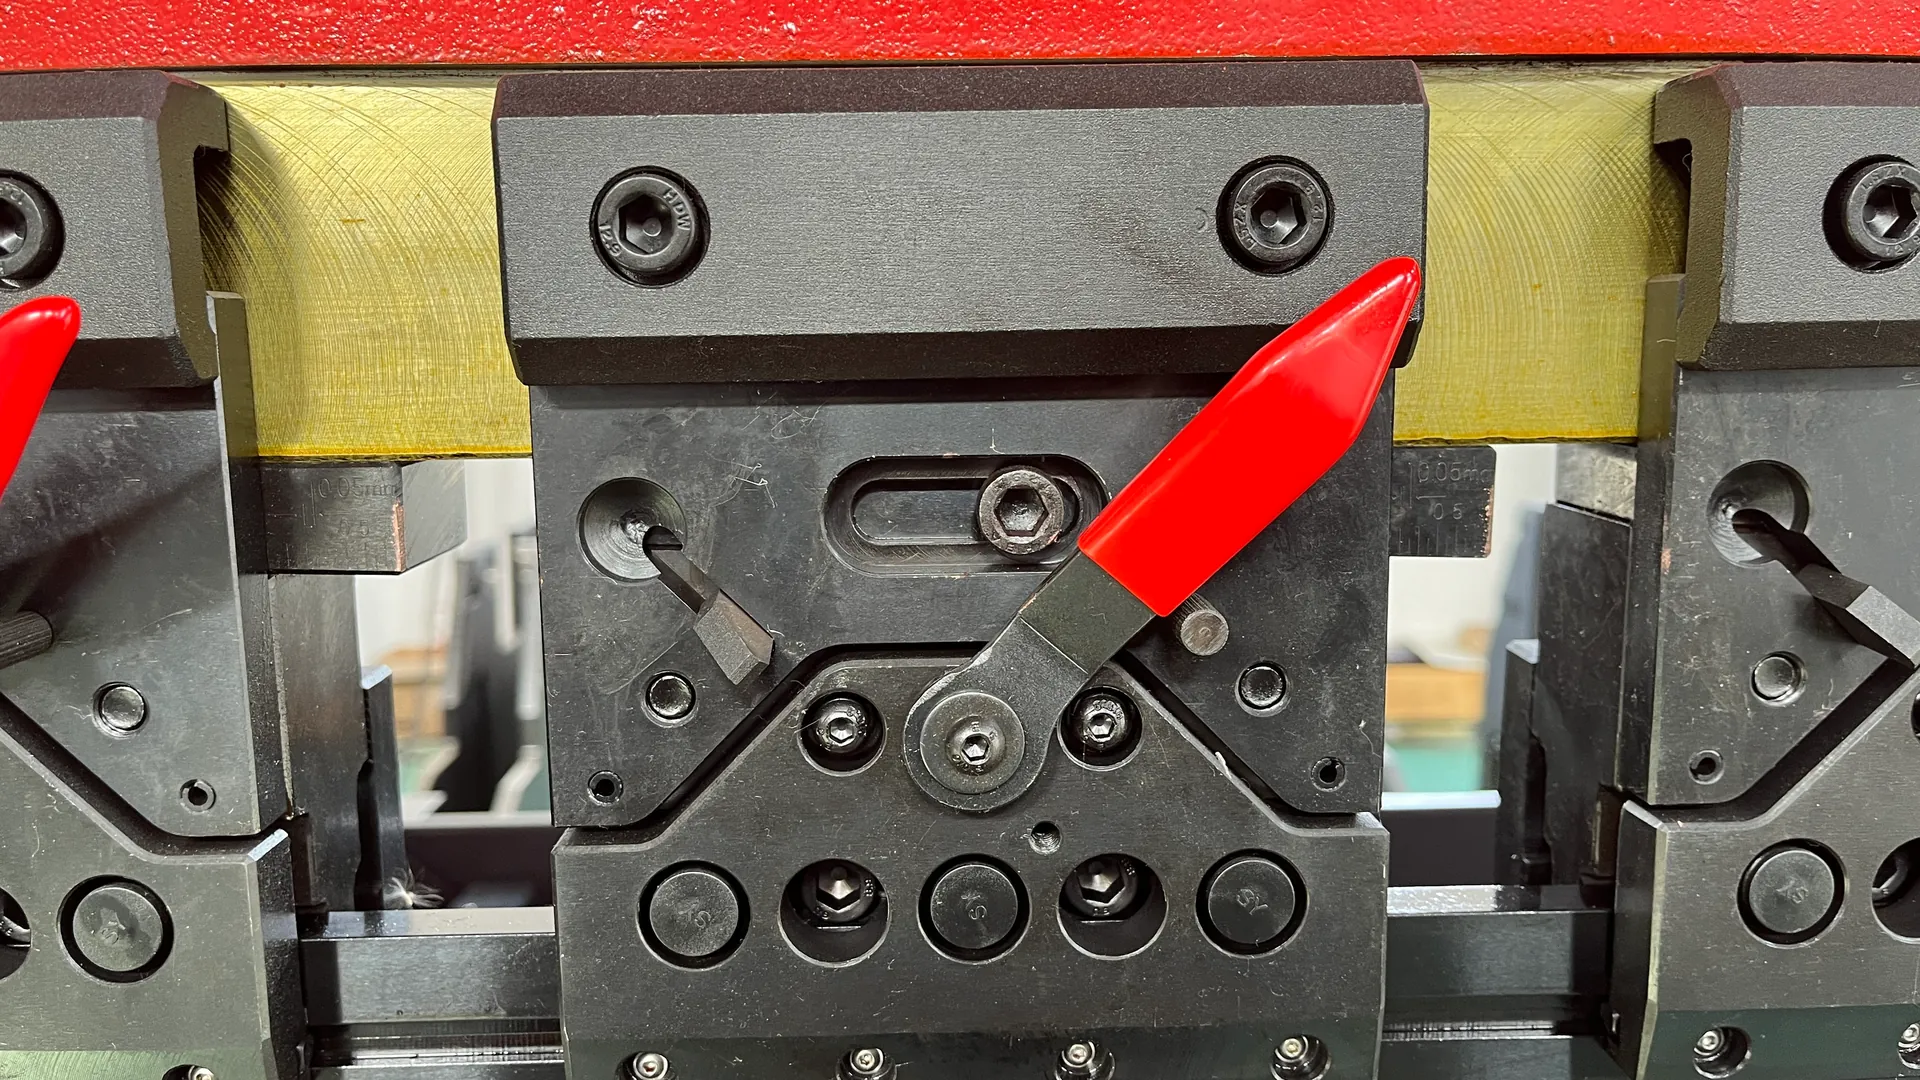
Changeover often matters more than ram speed in a mixed workshop. Time the work from the last accepted part of one job to the first accepted part of the next.
The operator’s role also changes:
- Torsion bar machines can suit a stable job with an experienced setter. More part changes can mean more manual adjustment and first-part correction.
- Electro-hydraulic machines usually need more controller training. Stored programs can then make repeat jobs easier to recall, although first-part checks are still needed.
Cost and Maintenance
A torsion bar press brake usually has a lower purchase price. An electro-hydraulic machine usually costs more because it adds control components and often more CNC functions.
The better purchase depends on your use. A lower-priced machine can cost more over time if changeovers keep it waiting. A higher-priced machine adds little if it makes one simple part all day.
Both machines need hydraulic maintenance. On a torsion bar machine, also inspect the shaft linkage and alignment. On an electro-hydraulic machine, ask which valves, feedback parts and controller items should be stocked. Our spare parts guide can help you prepare that list.
Which Machine Fits Your Work?
| Your work | Better starting point | Why |
|---|---|---|
| Repeated brackets and channels | Torsion bar | The setup can stay stable |
| Cabinet sides with return flanges | Electro-hydraulic | Sequences and gauge positions change more often |
| Long stainless panels | Electro-hydraulic | Side-to-side correction helps; still check crowning |
| Small shop with few part changes | Torsion bar | Lower investment may match the workload |
| Many small batches each shift | Electro-hydraulic | Program recall can reduce repeated setup |
| Frequent off-center bends | Electro-hydraulic | Better suited, but check the load limits |
If you want to avoid a hydraulic drive completely, compare an electric press brake as well.
CHENDA Electro-Hydraulic Press Brake Models
The CHENDA catalog lists electro-hydraulic CNC press brakes and no torsion bar models. All four CHD models share a 3,200 mm bending length, 2,700 mm distance between uprights, 400 mm throat depth, 200 mm slider travel, 420 mm die loading height and 800 mm worktable height.
| Model | Nominal force, kN | Listed power, kW |
|---|---|---|
| CHD-100T/3200 | 1,000 | 7.5 |
| CHD-200T/3200 | 2,000 | 15 |
| CHD-250T/3200 | 2,500 | 15 |
| CHD-320T/3200 | 3,200 | 18.5 |
The catalog describes these CHD features:
- Standard mechanical deflection compensation, with the amount adjusted automatically by the CNC
- A back gauge with multiple axes available as options
- An integrated hydraulic control system imported from Germany
- A welded machine body with overall tempering for stress relief
Review our electro-hydraulic synchronized CNC press brakes or browse the press brake range. Confirm the configuration on your quotation.
How to Test Both Machines
Use the same drawing, material batch, tooling plan and measuring method. Then compare:
- Bend angle at both ends and the middle of a long part
- Flange length across several repeated parts
- Time from the previous job to the first accepted part
- Short-flange access and any tool or gauge collision
- Operator steps after a change of material batch
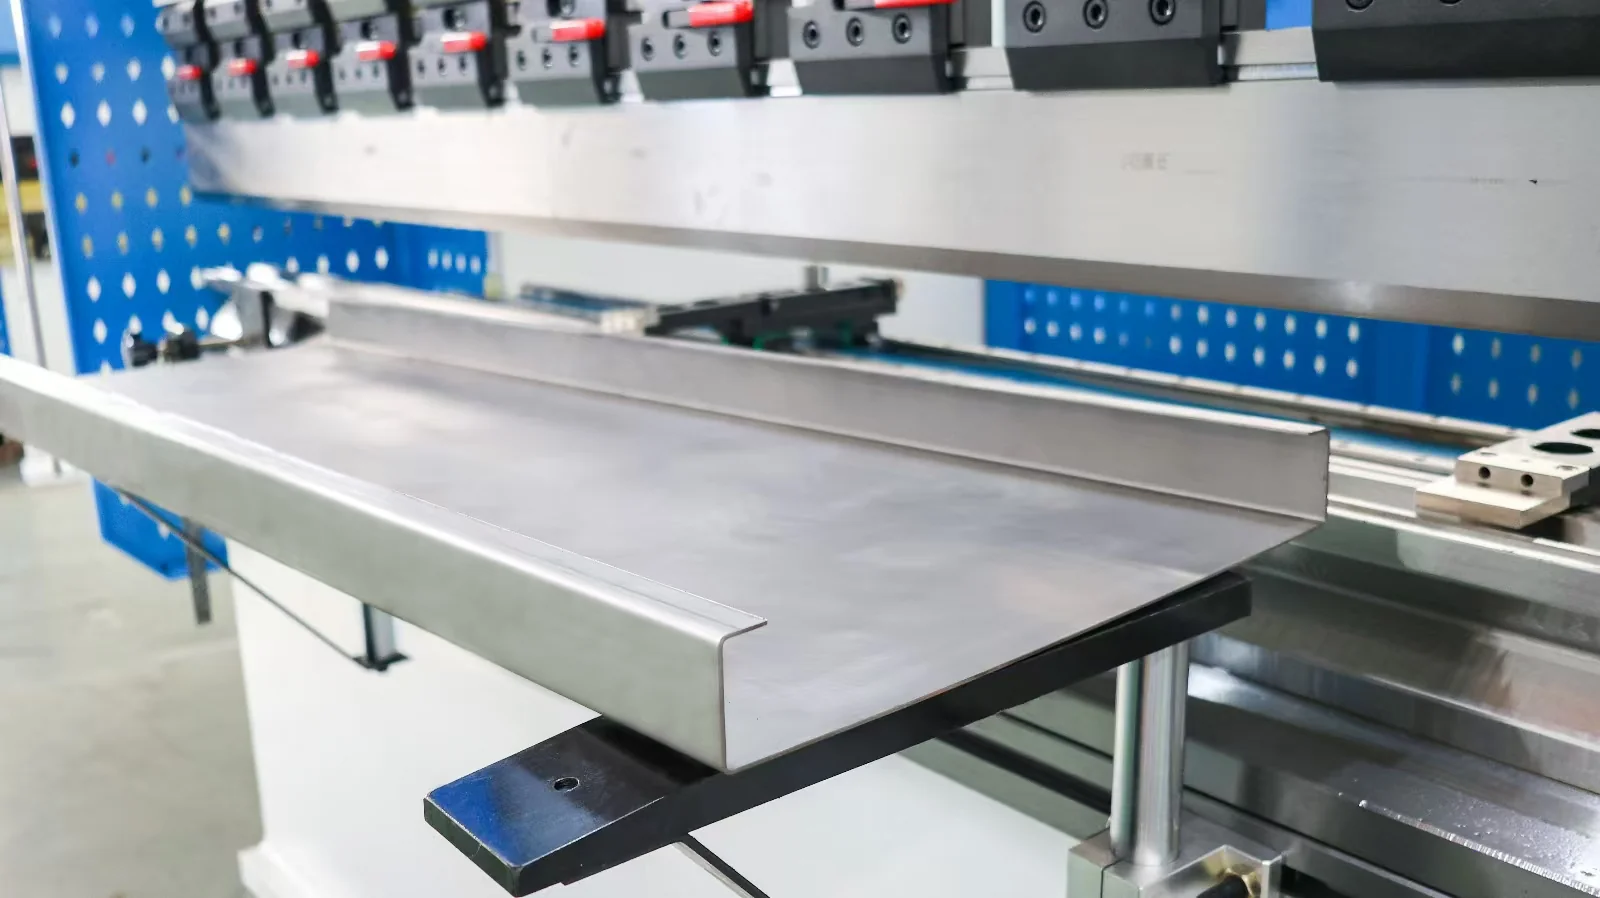
This shows how each machine handles your work. A short demonstration on an easy part cannot show that.
Frequently Asked Questions
Is an NC press brake the same as a torsion bar press brake?
Often, but not always. Suppliers use these labels differently, and a torsion bar machine can have a CNC-style controller. Confirm the ram synchronization method.
Is a torsion bar press brake good for stainless steel?
It can bend stainless steel within the machine and tool capacity. Stainless usually needs more force and can show more springback, so test your grade and thickness.
Does electro-hydraulic control remove springback?
No. It controls ram position. Springback still depends on the material and bending conditions.
Can I start with a torsion bar machine and upgrade later?
Plan for a new machine rather than assuming the ram system can be upgraded. If you expect more part changes soon, compare both machines against your future workload now.
Which machine should a small workshop buy?
Start with the part mix. A torsion bar machine can suit a few stable jobs. Electro-hydraulic control becomes more useful as part changes and accuracy demands increase.
Request a Press Brake Recommendation
Send the part drawing, material grade, thickness, bend length, target angles, batch size and destination country. CHENDA can then review whether a CHD electro-hydraulic press brake fits your work.
Get a press brake quote or email info@chendalaser.com.