Jump to a section
- 1. How Each Drive Works
- 2. Energy Use: Real Numbers
- 3. How to Calculate Press Brake Tonnage
- 4. Choose a CHENDA Model from the Table
- 5. Die Opening, Radius and Minimum Flange
- 6. Accuracy: Electric vs Hydraulic
- 7. Productivity
- 8. Total Cost of Ownership
- 9. Which Machine for Which Work?
- 10. Safety
- 11. Acceptance Test Checklist
- Frequently Asked Questions
- Request a CHENDA Press Brake Recommendation
Quick answer:
- Energy: An all-electric press brake uses much less energy, mainly because it draws almost nothing while idle. One manufacturer’s figures put an 80-ton machine at about 2,200 kWh a year electric vs 5,000 kWh hydraulic on a single shift — 56% less.
- Money: At 2025 EU business electricity prices, that saving is worth only about €510–630 a year.
- The real choice: Pick electric press brakes for fast, repetitive small parts up to about 100–300 tons. Pick electro-hydraulic CNC for longer bends, thicker plate and higher tonnage.
| All-electric | Electro-hydraulic CNC | |
|---|---|---|
| Force generation | Servo motors + ball screws or belts | Hydraulic cylinders, CNC-synchronized (Y1/Y2) |
| Annual energy, 80 t, one shift | about 2,200 kWh | about 5,000 kWh |
| Idle consumption | Near zero | Pump losses (standby can be up to 90% of time) |
| Typical size range | Small to mid (servo-electric up to about 300 t) | Small to very large |
| Maintenance | No hydraulic oil, seals or filters | Oil, filters, seals, valves |
| Best for | Repeated brackets, enclosures, small panels | Long bends, thick plate, mixed work |
Scroll horizontally to view all columns on smaller screens
Source for energy figures: a manufacturer comparison reported by an industry publication.
Not sure which drive or tonnage you need? Send CHENDA your thickest material, longest bend and one drawing. We will calculate the tonnage and recommend a machine. Request a Press Brake Recommendation · Email info@chendalaser.com · Phone +86 153 0644 7102
1. How Each Drive Works
All-electric press brake: Servo motors drive the ram through ball screws or a belt-and-pulley system. Motors run only when the ram moves, so idle power is very low.
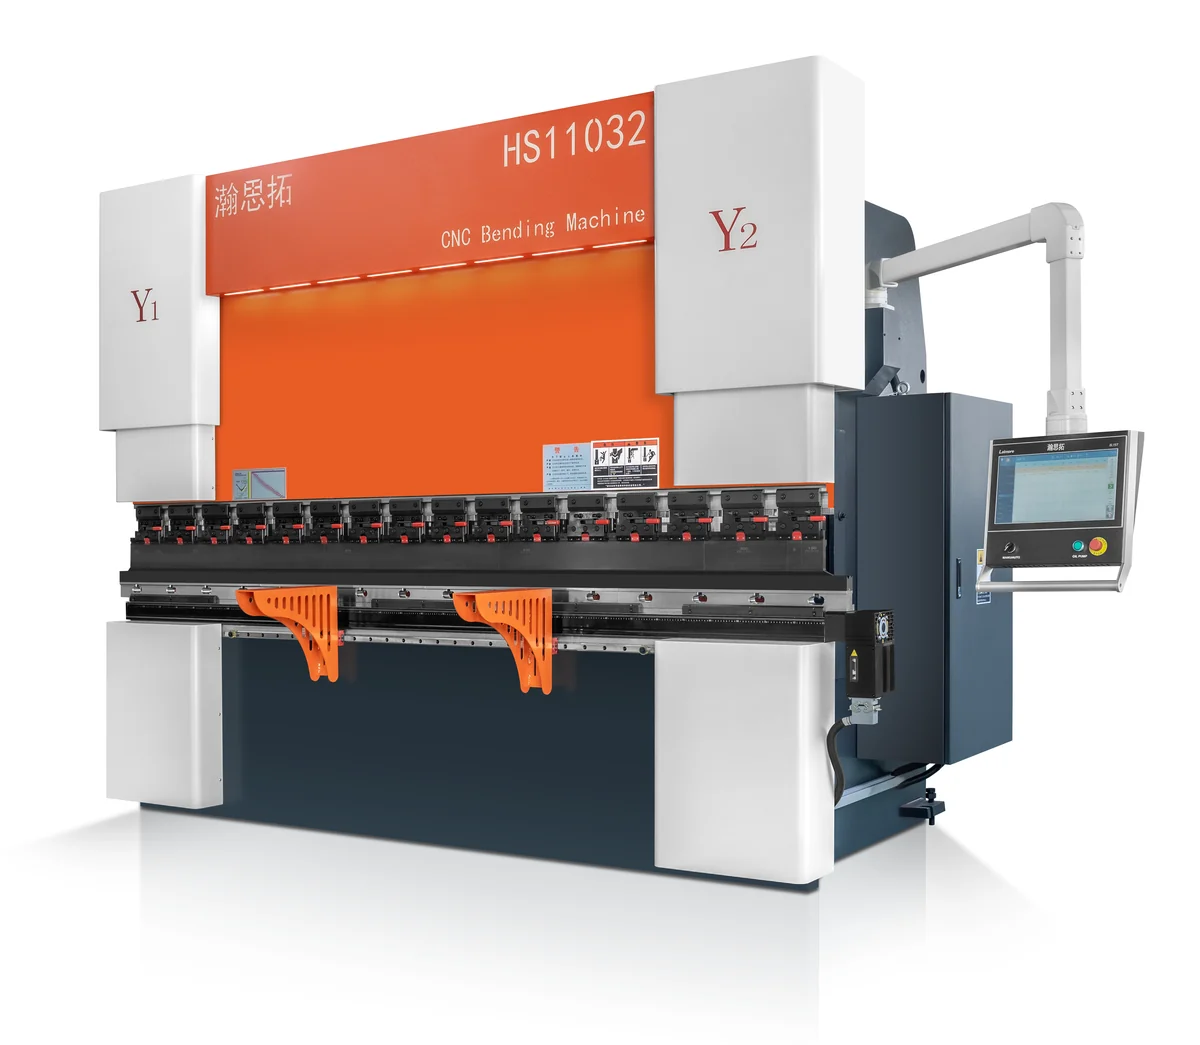
Electro-hydraulic CNC press brake: A hydraulic pump drives two cylinders (Y1 and Y2). A CNC synchronizes them using linear scale feedback.
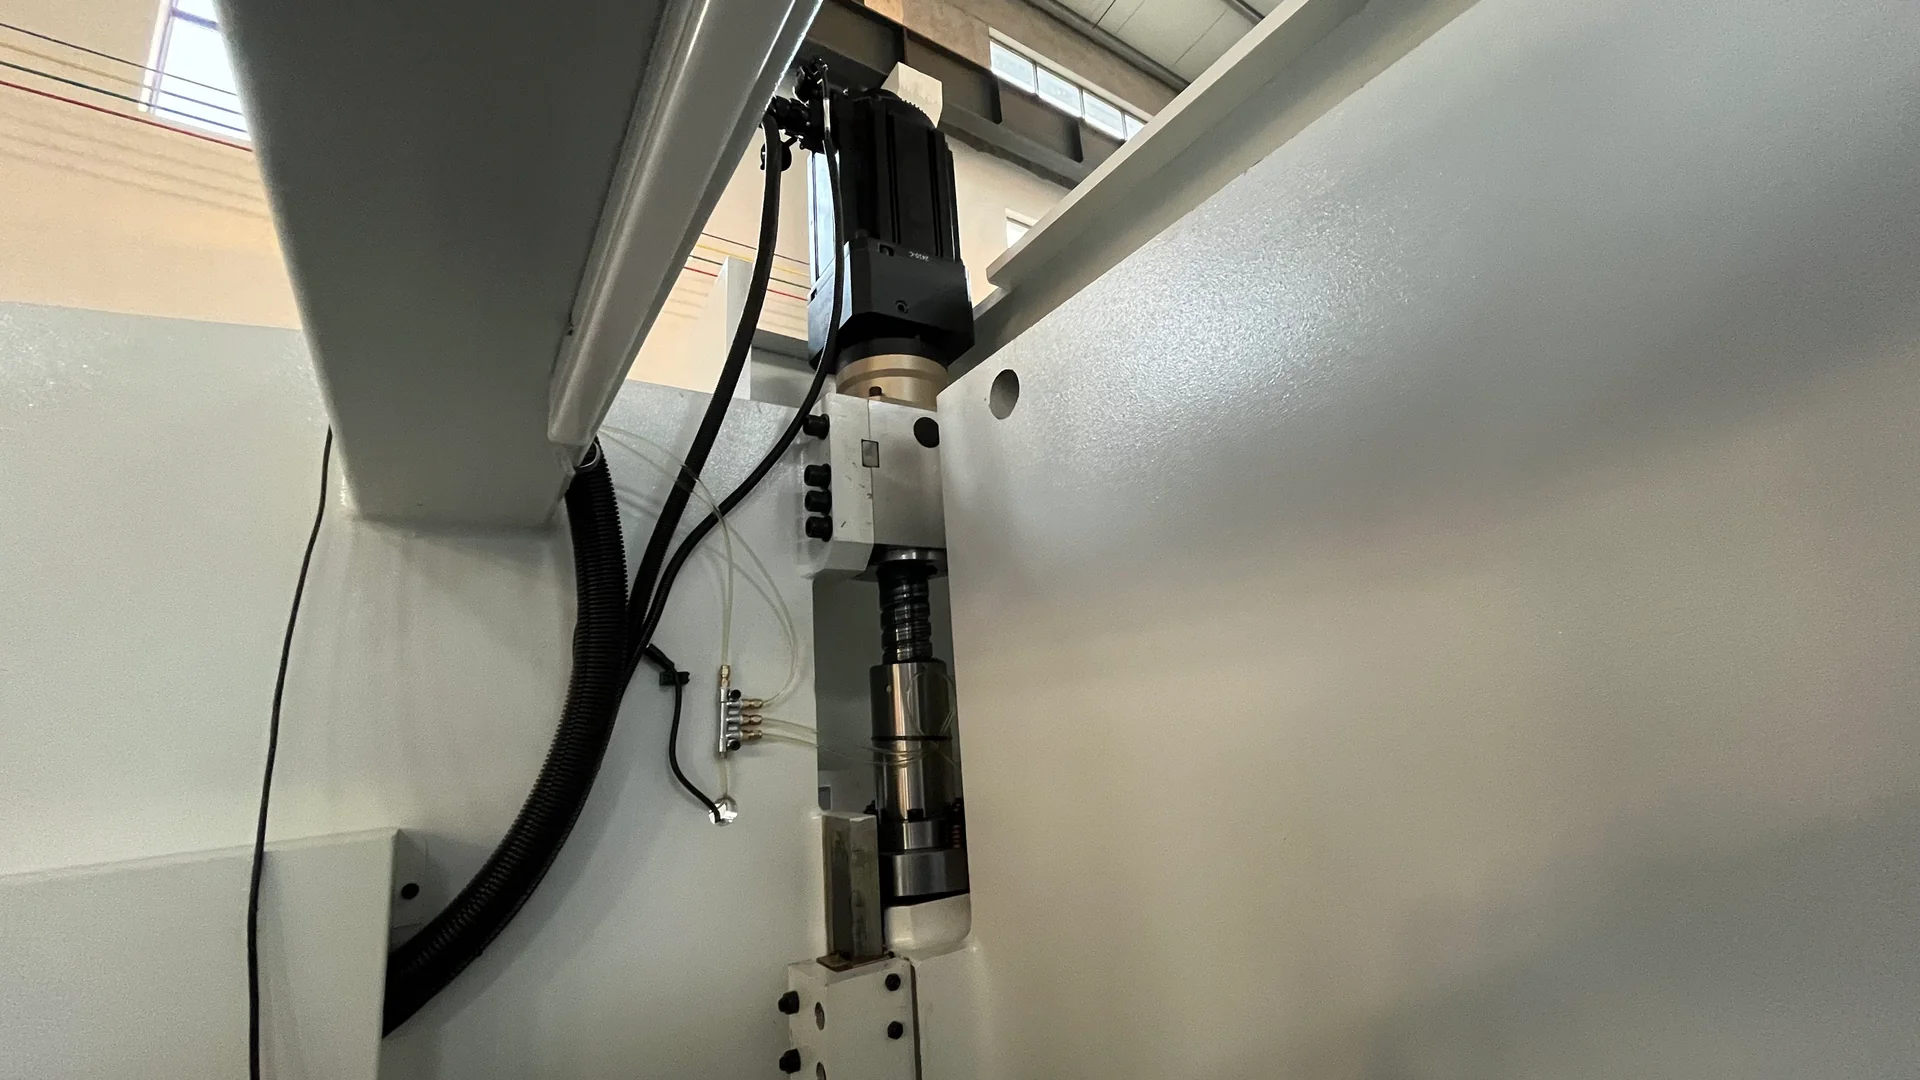
Servo-hydraulic (hybrid): Hydraulic cylinders, but the pump is driven by a variable-speed servo motor. This is not an all-electric machine, but it cuts energy too. A 2022 study on an 80-ton press brake measured 54% energy saving over 100 cycles compared with a valve-controlled hydraulic system (Uludağ University study).
2. Energy Use: Real Numbers
Illustrative manufacturer-published annual energy consumption (single shift, not a CHENDA energy guarantee):
| Machine | Annual energy |
|---|---|
| Hydraulic press brake, 80 t | 5,000 kWh |
| Electric press brake, 80 t | 2,200 kWh |
| Electric press brake, 150–200 t | 3,960 kWh |
Scroll horizontally to view all columns on smaller screens
Most of the difference comes from standby: press brakes can sit idle up to 90% of the time, and a hydraulic pump keeps drawing power. The bigger the hydraulic machine, the bigger the pump and the greater the loss.
What is the saving worth?
2,800 kWh saved per year (80 t, one shift):
| Electricity price (Eurostat, non-household, H2 2025) | Annual saving |
|---|---|
| EU average €0.1837/kWh | about €514 |
| Germany €0.2264/kWh | about €634 |
Scroll horizontally to view all columns on smaller screens
Double it for two shifts.
Bottom line: Energy alone rarely pays for an electric machine. Faster cycles, less maintenance and no oil are usually the bigger reasons.
3. How to Calculate Press Brake Tonnage
A published air-bending formula for mild steel (60,000 psi tensile):
Tonnage (US tons) = [575 × t² ÷ V ÷ 12] × bend length (t, V and length in inches)
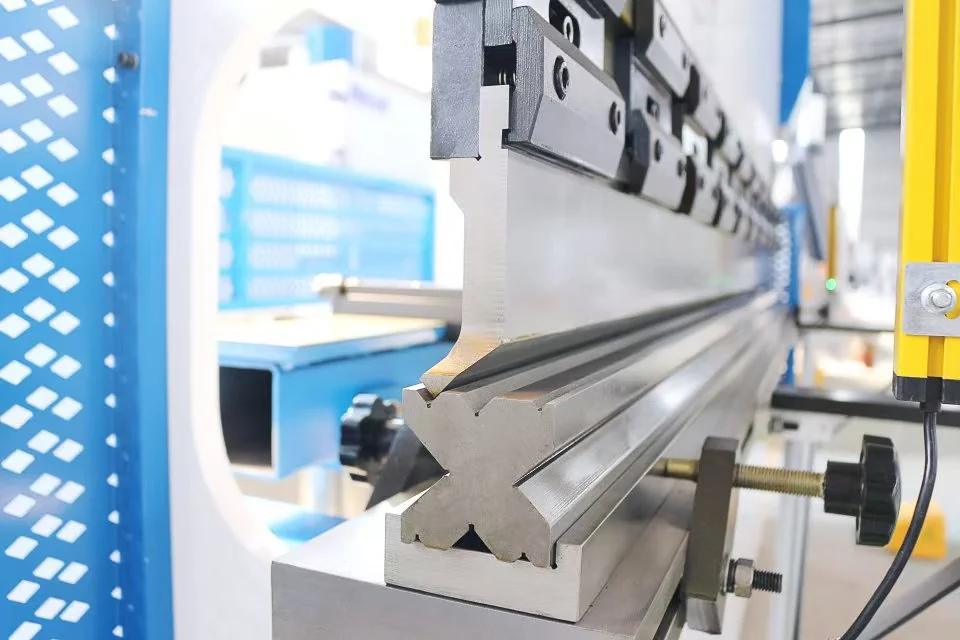
Converted to metric, this is about:
Force (kN per metre of bend) ≈ 660 × t² ÷ V
Here t is the thickness in mm and V the die opening in mm. Then multiply by the material factor (tensile strength ÷ 414 MPa).
| Material | Tensile strength | Factor |
|---|---|---|
| Mild steel (reference) | 414 MPa (60,000 psi) | 1.0 |
| Stainless 304 (ASTM A240 minimum) | 515 MPa | about 1.24 |
| Aluminium 5052-H32 | about 215–265 MPa | about 0.5–0.65 |
Scroll horizontally to view all columns on smaller screens
Bottoming needs about 5× the air-bending force, and coining 10× or more.
The tonnage formula is an engineering reference for air bending under stated assumptions. Confirm the final selection using actual tooling charts and machine ratings.
Tonnage table (air bending, V = 8 × t, full 3.2 m bend)
| Thickness | Mild steel kN/m | Mild steel, 3.2 m | Stainless 304 kN/m | Stainless 304, 3.2 m |
|---|---|---|---|---|
| 2 mm | 165 | 528 kN | 205 | 657 kN |
| 3 mm | 248 | 792 kN | 308 | 985 kN |
| 4 mm | 330 | 1,056 kN | 411 | 1,314 kN |
| 6 mm | 495 | 1,584 kN | 616 | 1,970 kN |
| 8 mm | 660 | 2,112 kN | 821 | 2,627 kN |
| 10 mm | 825 | 2,640 kN | 1,026 | 3,284 kN |
Scroll horizontally to view all columns on smaller screens
Rule of thumb: Doubling the thickness doubles the force when you also double the die opening. If the die stays the same, the force quadruples.
Add 20–30% margin so the machine is not working at its limit.
4. Choose a CHENDA Model from the Table
CHENDA electro-hydraulic CNC press brakes (published catalogue values):
| Model | Force | Bending length | Distance between uprights | Throat depth | Stroke | Table height | Main motor |
|---|---|---|---|---|---|---|---|
| CHD-100T/3200 | 1,000 kN | 3,200 mm | 2,700 mm | 400 mm | 200 mm | 800 mm | 7.5 kW |
| CHD-200T/3200 | 2,000 kN | 3,200 mm | 2,700 mm | 400 mm | 200 mm | 800 mm | 15 kW |
| CHD-250T/3200 | 2,500 kN | 3,200 mm | 2,700 mm | 400 mm | 200 mm | 800 mm | 15 kW |
| CHD-320T/3200 | 3,200 kN | 3,200 mm | 2,700 mm | 400 mm | 200 mm | 800 mm | 18.5 kW |
Scroll horizontally to view all columns on smaller screens
Source: CHENDA electro-hydraulic CNC press brakes.
Matching the tonnage table to models (full 3.2 m bends):
| Your thickest full-length bend | Suggested model |
|---|---|
| Mild steel up to 3 mm, stainless up to 2 mm | CHD-100T/3200 |
| Mild steel 4–6 mm, stainless 3–4 mm | CHD-200T/3200 |
| Stainless 6 mm | CHD-250T/3200 |
| Mild steel 8–10 mm, stainless 8 mm | CHD-320T/3200 |
Scroll horizontally to view all columns on smaller screens
The table keeps at least 20% spare capacity at full bend length.
Shorter bends need proportionally less force. A 1 m bend in 8 mm mild steel needs only about 660 kN.
Send us your thickest part. CHENDA will check tonnage, die opening, flange length and tool clearance, and confirm the right model. Check My Tonnage · info@chendalaser.com
5. Die Opening, Radius and Minimum Flange
- V-die opening: a common starting point is about 8 × material thickness. Smaller V means more force and a tighter radius.
- Inside radius: in air bending, roughly 15–17% of the V opening for mild steel.
- Minimum flange: the flange must reach across the die shoulder; short flanges need a narrower V and therefore more force.
Deep boxes also need ram stroke, daylight, throat depth and tool height checked — force alone does not guarantee the part can be made.
6. Accuracy: Electric vs Hydraulic
Neither drive is automatically more accurate. Finished-part accuracy depends on:
- Ram positioning repeatability (servo or Y1/Y2 hydraulic with linear scales)
- Crowning to compensate for frame and tool deflection on long bends
- Material variation in thickness, strength and springback
- Tooling wear
- Angle measurement, if fitted
Ask for finished-part tolerances on your material, not just axis repeatability.
7. Productivity
Electric machines usually have faster approach and return strokes and quick reversals, which helps on short, repeated bends. On long, heavy parts, part handling is the limit and drive speed matters less.
Compare accepted parts per hour on a real part family, not catalogue speeds.
8. Total Cost of Ownership
| Cost | Electric | Electro-hydraulic |
|---|---|---|
| Purchase price | Usually higher per ton | Usually lower per ton |
| Energy | About 50–60% less in the examples above | Higher, mainly standby |
| Hydraulic oil and filters | None | Periodic replacement |
| Seals and valves | None | Wear items |
| Mechanical drive | Ball screws, belts, bearings | Cylinders, pump |
| Size range | Small to mid tonnage | All sizes |
Scroll horizontally to view all columns on smaller screens
9. Which Machine for Which Work?
| Application | Better fit |
|---|---|
| Electrical enclosures, brackets, small repeated parts | Electric |
| Stainless kitchen equipment, 1–3 mm, 1–3 m long | Either — compare cycle time |
| Machinery frames, 6–10 mm plate, 3 m bends | Electro-hydraulic (CHD-250T/320T) |
| High-mix job shop | Either — focus on controller, tooling and backgauge |
Scroll horizontally to view all columns on smaller screens
10. Safety
Press brakes create crushing hazards at the tools. Specify light curtains or laser guarding, emergency stops, two-hand or foot-pedal controls with safe-speed changeover, and operator training.
References: OSHA — Powered press brakes; ANSI B11.3-2022.
11. Acceptance Test Checklist
- Bend your own material grade and thickness.
- Measure angles at both ends and the middle of a long bend.
- Make a complete box or bracket, not just one bend.
- Time the full part cycle.
- Record energy over a defined job if energy matters.
Frequently Asked Questions
Is an electric press brake more energy-efficient?
Yes. One manufacturer reports 2,200 kWh a year for an 80 t electric machine vs 5,000 kWh for hydraulic on a single shift — about 56% less.
How much money does an electric press brake save on energy?
About €510–630 a year for an 80 t machine on one shift at 2025 EU business electricity prices. Two shifts roughly double it.
How do I calculate press brake tonnage?
For mild steel in air bending, force ≈ 660 × t² ÷ V kN per metre (t and V in mm). Multiply by about 1.24 for stainless 304 and about 0.5–0.65 for 5052 aluminium.
What tonnage do I need for 6 mm mild steel 3 m long?
With V = 48 mm, about 495 kN/m, so about 1,600 kN for 3.2 m. A CHD-200T/3200 (2,000 kN) covers it with margin.
Is an electric press brake more accurate?
Not automatically. Accuracy depends on positioning, crowning, tooling and material as much as on the drive.
Is a servo-hydraulic press brake the same as electric?
No. It still uses hydraulic cylinders, but a servo-driven pump cuts energy — one study measured 54% savings.
Which press brake is better for thick plate?
Electro-hydraulic CNC machines, because they scale to high tonnage at lower cost.
Request a CHENDA Press Brake Recommendation
Send us:
- Material grades and thickness range
- Longest bend and one drawing
- Typical batch sizes and tolerances
- Country of installation
We will calculate tonnage and recommend the drive and model.
Explore CHENDA Press Brakes · Request a Technical Equipment Quote
Email: info@chendalaser.com · Phone: +86 153 0644 7102