Jump to a section
- 1. How Much Can a Handheld Laser Weld? Thickness by Power
- 2. Speed: Why Faster Welding Is Not the Same as Faster Production
- 3. Price of Handheld Laser Welders
- 4. Weld Quality: Is Laser Stronger?
- 5. Fit-Up: The Biggest Difference
- 6. Running Costs Compared
- 7. Which Process for Which Product?
- 8. When Not to Switch to Laser
- 9. Safety: Non-Negotiable
- 10. CHENDA Handheld Laser Welders
- 11. Questions to Ask Before Buying
- Frequently Asked Questions
- Request a Handheld Laser Welding Recommendation
Quick answer:
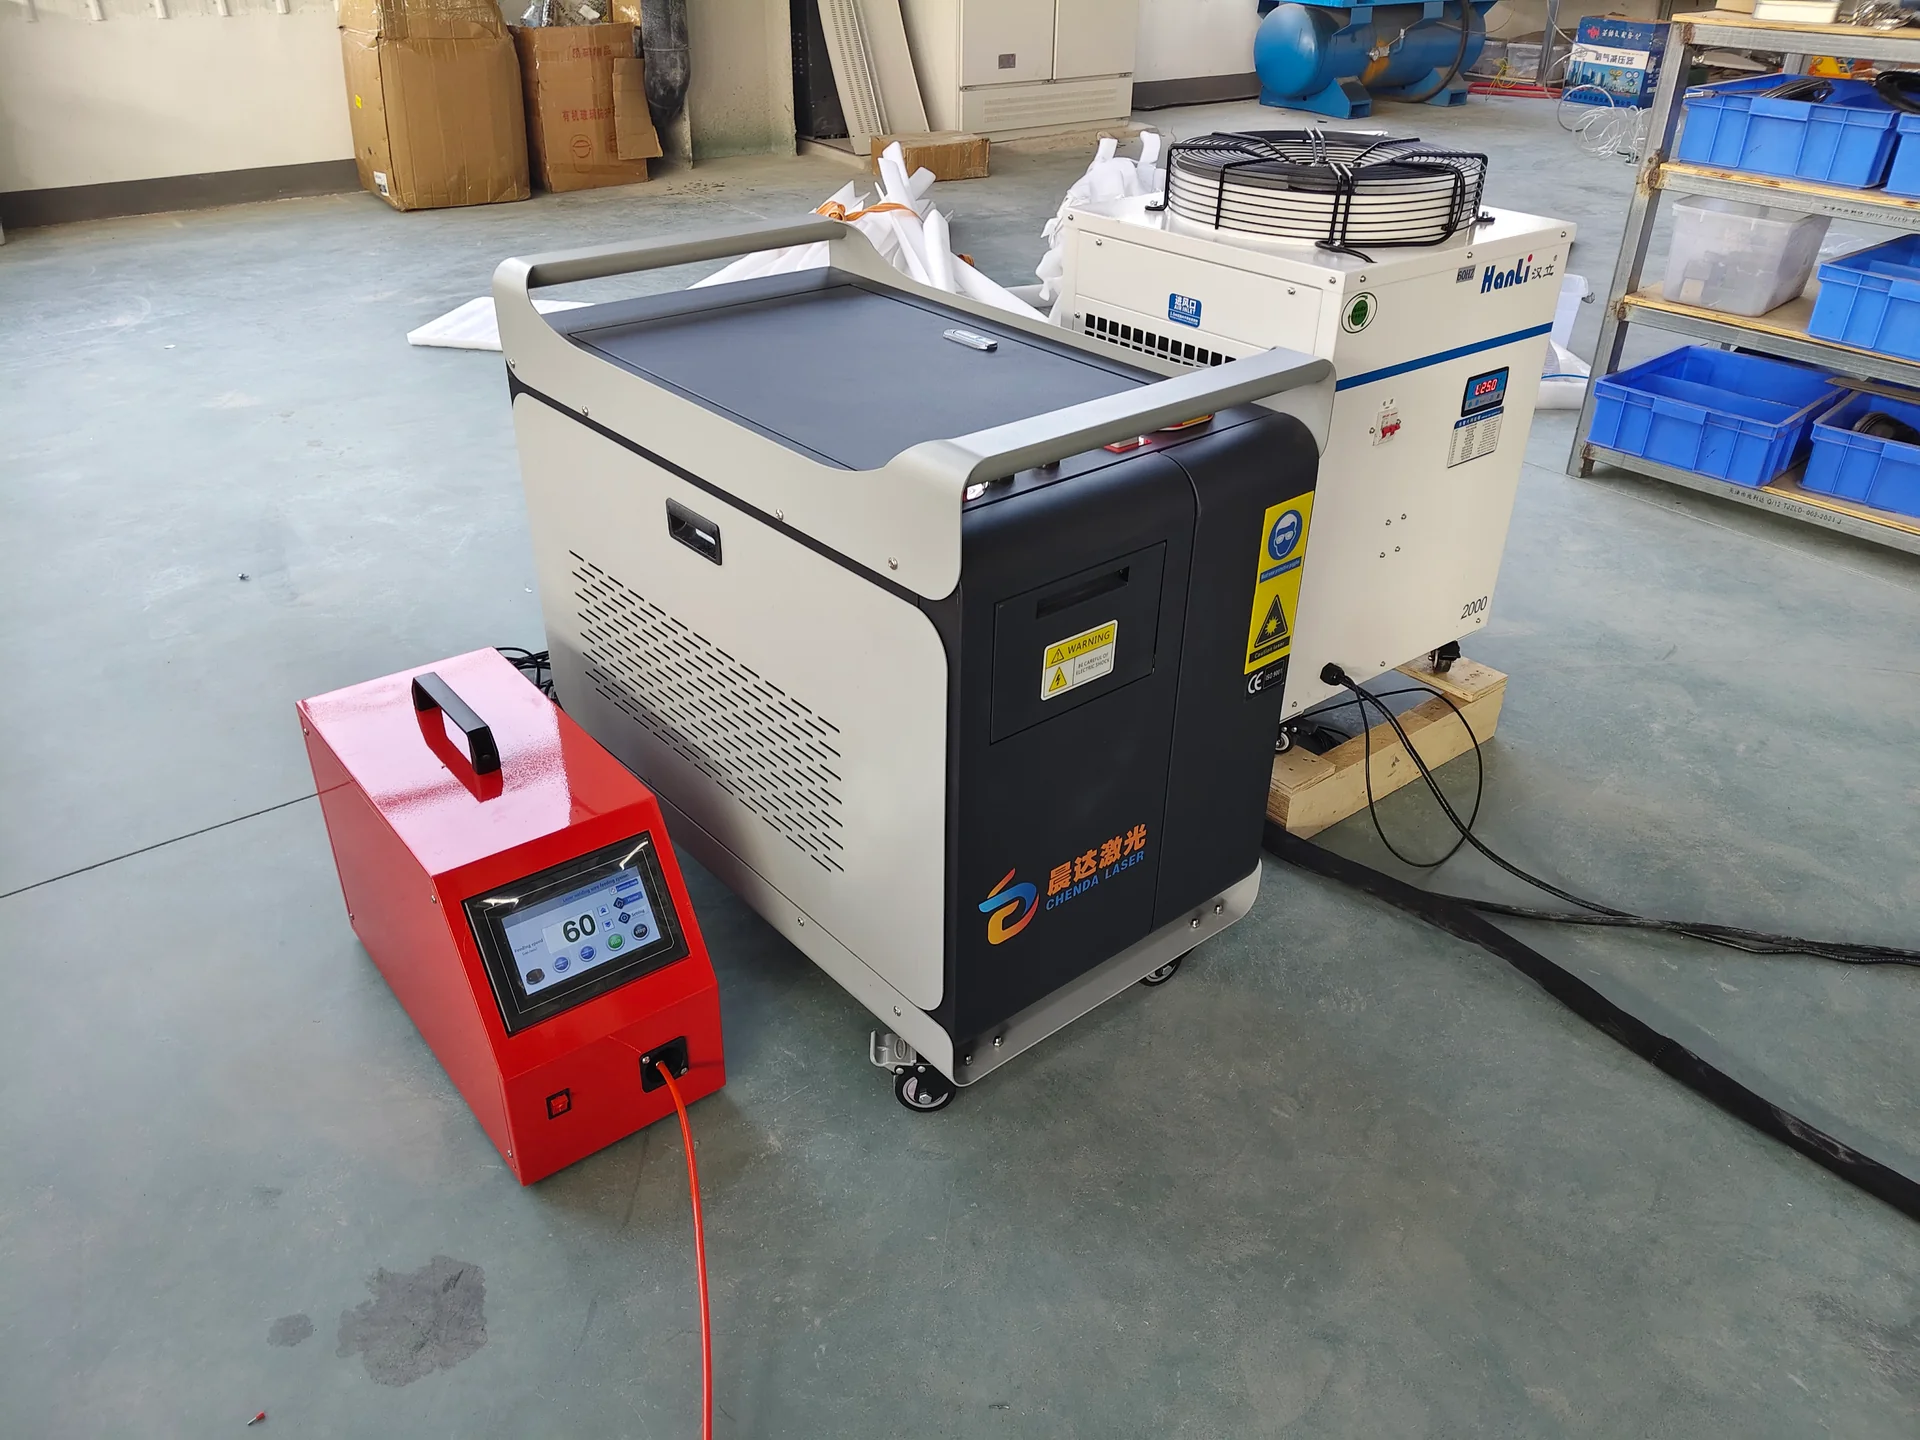
- Speed: Handheld laser welding can be up to 4× faster than TIG or MIG on suitable seams (manufacturer-published example for a specific handheld laser system).
- Thickness: A 1,500 W unit welds about 4 mm single-side in stainless steel, mild steel and aluminium, and up to about 10 mm welded from both sides. Copper is limited to about 1 mm.
- Price: Chinese handheld laser welders are listed at about US$1,600–7,900.
- When it fits: It is best for thin to medium sheet with tight, consistent fit-up: cabinets, enclosures, furniture and kitchen equipment.
- When it does not: MIG stays better for thick structural fillets and gappy joints. TIG stays better for critical manual work.
| Handheld laser | TIG | MIG/MAG | |
|---|---|---|---|
| Speed | Up to 4× TIG/MIG on suitable seams | Slowest | Fast, high deposition |
| Heat input / distortion | Low | Medium | Medium–high |
| Fit-up tolerance | Tight (wire feed helps) | Flexible | Most flexible |
| Typical thickness | about 0.5–4 mm single-side at 1.5 kW | Thin to medium | Medium to thick |
| Finishing | Often little grinding | Clean | Spatter cleanup common |
| Skill to learn | Short | Long | Medium |
| Safety | Class 4 laser — controlled area required | Arc radiation, fumes | Arc radiation, fumes, spatter |
Scroll horizontally to view all columns on smaller screens
Want to know if laser welding suits your parts? Send CHENDA a photo or drawing of the joint, the material and thickness. We will recommend the laser power and wire set-up. Request a Welding Recommendation · Email info@chendalaser.com · Phone +86 153 0644 7102
1. How Much Can a Handheld Laser Weld? Thickness by Power
| Laser power | Steel (stainless / mild), single-side | Interpretation |
|---|---|---|
| 1,000 W | about 3 mm | Illustrative claim; validate for the actual joint |
| 1,500 W | about 4 mm (aluminium also about 4 mm; copper about 1 mm) | Specific 1,500 W system example, not universal capacity |
| 1,500 W, welded from both sides | up to about 10 mm (steel, aluminium) | Specific-system example; two-sided access required |
| 1,500 W | up to 5 mm (vendor claim) | Published claim; confirm through an application trial |
| 2,000 W | up to about 8 mm (vendor claim) | Published claim; confirm through an application trial |
Scroll horizontally to view all columns on smaller screens
Welding thickness figures represent published system examples, not CHENDA performance guarantees. Capability depends on material, joint, penetration, passes and equipment configuration.
Treat higher vendor claims with caution: thickness depends on joint type, number of passes, filler wire and the required penetration. For a load-bearing joint, test and section a sample.
2. Speed: Why Faster Welding Is Not the Same as Faster Production
A manufacturer reports that its handheld laser welding system can weld up to 4× faster than MIG and TIG in suitable applications.
But the welding arc is only part of the job time. Example batch:
| Activity | TIG | Laser, 40% faster welding | Laser, 4× faster welding |
|---|---|---|---|
| Preparation and fixturing | 25 min | 25 min | 25 min |
| Welding | 40 min | 24 min | 10 min |
| Handling, inspection, finishing | 35 min | 35 min | 35 min |
| Total | 100 min | 84 min (−16%) | 70 min (−30%) |
Scroll horizontally to view all columns on smaller screens
The real gain is often in finishing. If laser welding removes grinding and straightening, the “handling and finishing” line shrinks too — that is where many sheet-metal shops see the biggest saving.
3. Price of Handheld Laser Welders
| Listing (supplier) | Power | Listed price (US$) |
|---|---|---|
| 1,500 W portable mini fiber laser welder, CE (public asking-price example) | 1,500 W | 1,680 – 4,800 |
| 4-in-1 welder (public asking-price example) | 1,500 / 2,000 W | 1,600 – 4,050 |
| 4-in-1 portable welder (public asking-price example) | 1,500 / 2,000 / 3,000 W | 2,500 |
| Air-cooled handheld welder (public asking-price example) | 800 – 2,000 W | 2,600 |
| Handheld fiber laser welder (public asking-price example) | 1,000 / 1,500 / 2,000 W | 5,800 – 6,800 |
| Portable welder for stainless and aluminium (public asking-price example) | — | 3,210 – 7,858 |
| Thick-plate water-cooled welder (public asking-price example) | — | 8,699 |
Scroll horizontally to view all columns on smaller screens
These prices are publicly advertised asking-price examples checked 19 October 2026, not CHENDA quotations. Equipment scope and delivery terms can differ.
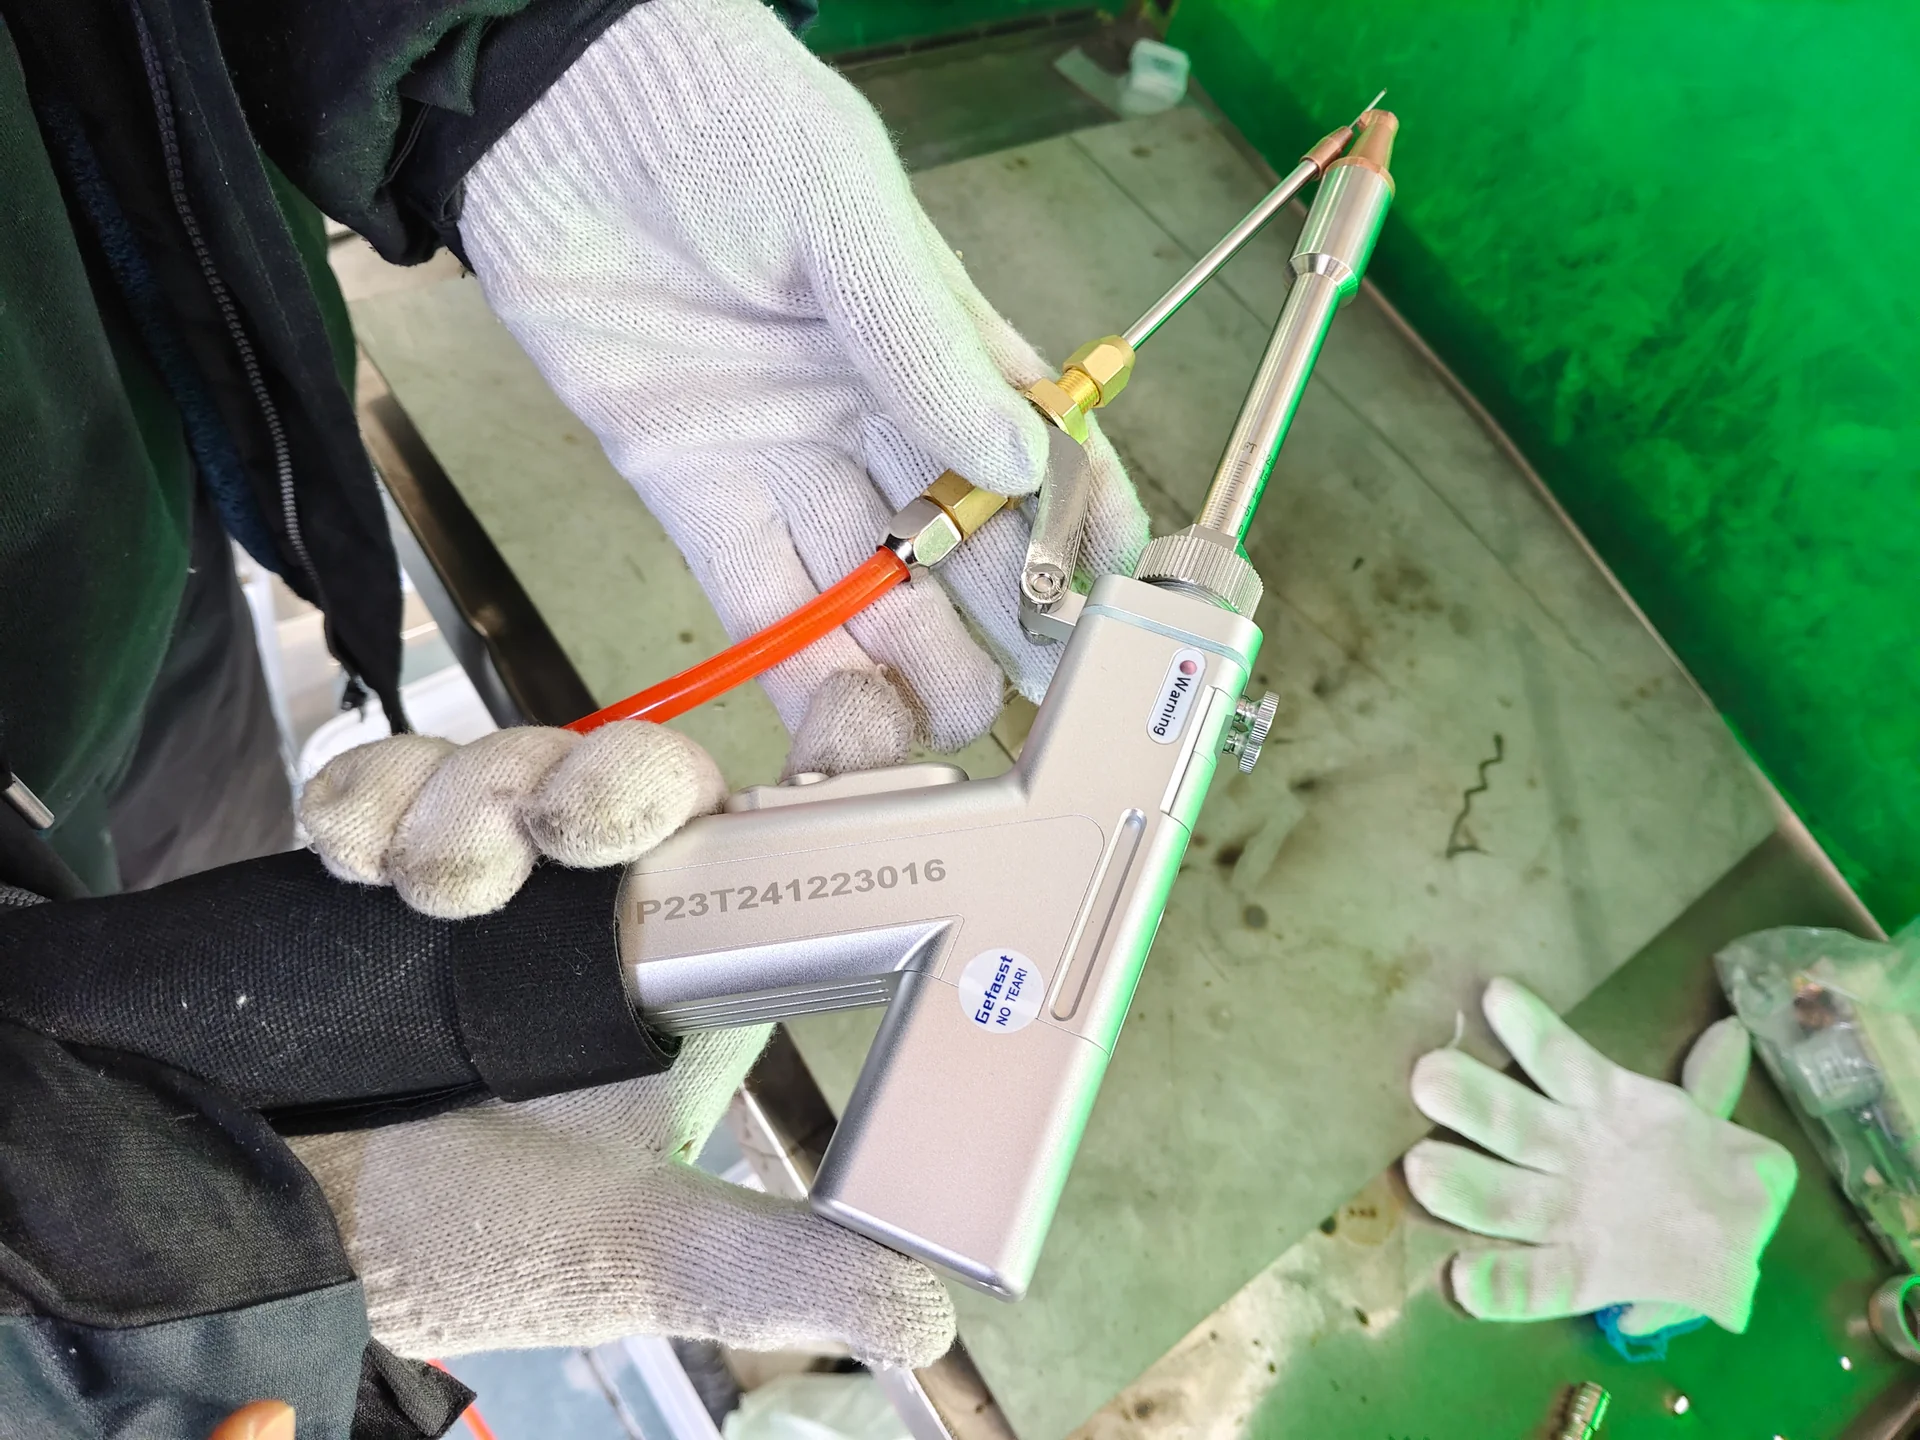
Price depends on laser source brand, cooling (air or water), wire feeder, head and wobble functions, and safety accessories. Budget separately for a laser-safe work area, laser-rated eyewear and fume extraction.
4. Weld Quality: Is Laser Stronger?
No process is stronger in every case. Strength depends on fusion, penetration, weld size and defects.
- Laser: narrow weld and small heat-affected zone; less distortion on thin sheet.
- TIG: precise control of the pool and filler; strong on critical and repair welds.
- MIG/MAG: deposits a lot of metal; best for large fillets on frames.
A clean-looking laser bead does not prove root fusion. For structural or pressure joints, use the qualified procedure and the test method your code requires (macro sections, bend tests, NDT).
5. Fit-Up: The Biggest Difference
A focused laser spot needs consistent gaps and alignment. TWI notes that laser welding is less tolerant of fit-up than arc welding. Clamping, wire feed and beam oscillation (wobble) improve tolerance.
| Joint | Laser | TIG / MIG |
|---|---|---|
| Accurately cut and bent sheet, tight corners | Excellent fit | Fine, but slower and more finishing |
| Variable gaps along the seam | Needs wire feed or better upstream cutting | MIG handles gaps best |
| Large fillet on thick plate | Limited | MIG |
| Repair work, unknown materials | Possible | TIG/MIG more flexible |
Scroll horizontally to view all columns on smaller screens
Source: TWI — Increasing laser welding tolerance to fit-up.
Tip: A precise fiber laser cutter and press brake upstream make laser welding much easier — good parts in, good welds out.
6. Running Costs Compared
| Cost | Handheld laser | TIG | MIG/MAG |
|---|---|---|---|
| Consumables | Protective lenses, nozzles, wire (if used) | Tungsten, filler, gas | Wire, tips, liners, gas |
| Shielding gas | Argon or nitrogen | Argon | Argon/CO₂ mixes |
| Labour per metre of weld | Lowest on suitable seams | Highest | Medium |
| Post-weld finishing | Often minimal | Low | Spatter and grinding |
| Facility | Laser-controlled area, extraction | Screens, extraction | Screens, extraction |
Scroll horizontally to view all columns on smaller screens
Compare cost per accepted assembly: total cost ÷ number of good parts, over the same period.
Thinking of replacing TIG on a product line? Send CHENDA a sample part. We will propose a laser welding trial and the equipment configuration. Arrange a Welding Trial · info@chendalaser.com
7. Which Process for Which Product?
| Product | Best first choice |
|---|---|
| Stainless steel cabinets and enclosures (1–3 mm) | Handheld laser |
| Commercial kitchen equipment | Handheld laser, TIG for special joints |
| Metal furniture | Laser for visible sheet seams; MIG for tube frames |
| Machinery frames (6 mm+) | MIG/MAG |
| Aluminium components | Laser or TIG — test the alloy |
| Repair and maintenance | TIG / MIG |
Scroll horizontally to view all columns on smaller screens
8. When Not to Switch to Laser
- Parts arrive with inconsistent gaps and upstream accuracy cannot be improved.
- Joints need large weld deposits.
- Critical joints have qualified TIG/MIG procedures and no time to re-qualify.
- You cannot set up a laser-controlled area.
- Too few suitable jobs to keep the machine busy.
9. Safety: Non-Negotiable
Industrial handheld laser welders are Class 4 lasers. Direct and reflected beams can cause severe eye and skin injury, and the near-infrared beam is invisible.
Requirements:
- A laser-controlled area with laser-rated barriers, curtains or a booth
- Laser-rated eyewear for the exact wavelength (welding helmets are not enough)
- A Laser Safety Officer or responsible person and trained operators
- Fume extraction — laser welding is not fume-free, especially on coated or stainless steel
Standards: ISO 11553-2:2026 for handheld laser processing machines (published August 2026), IEC 60825-1, and ANSI Z136.1 / Z136.9 in the US.
Sources: AWS — Handheld laser welding safety; ISO 11553-2:2026; NIOSH — welding ventilation.
10. CHENDA Handheld Laser Welders
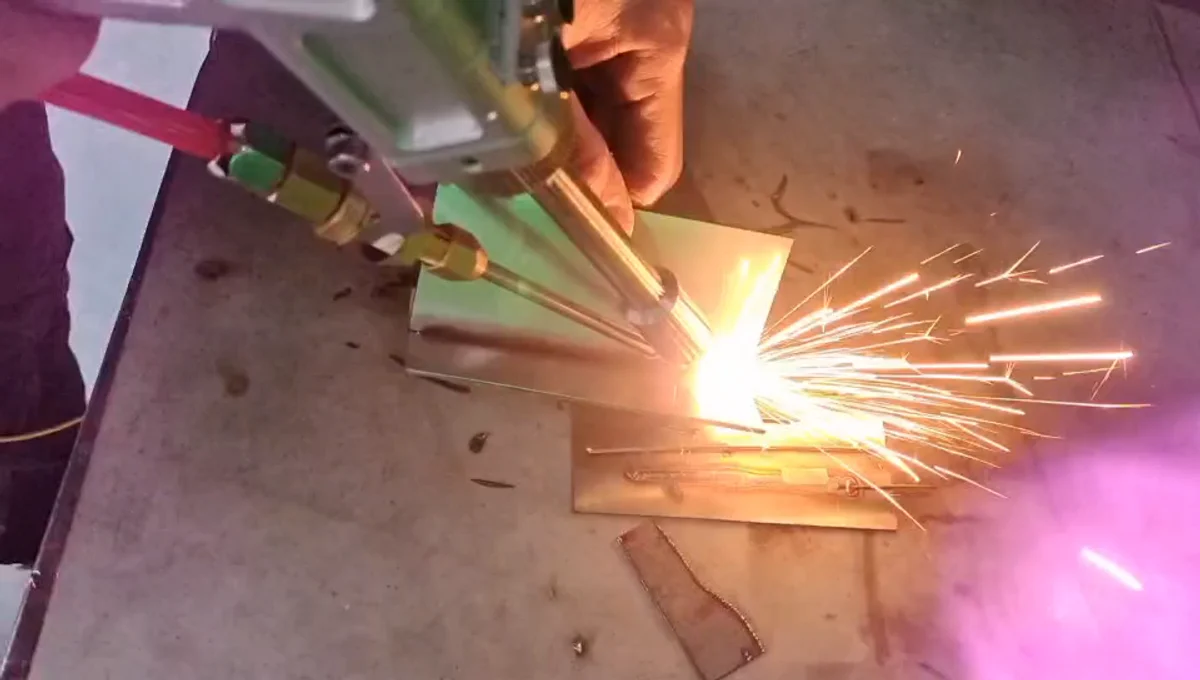
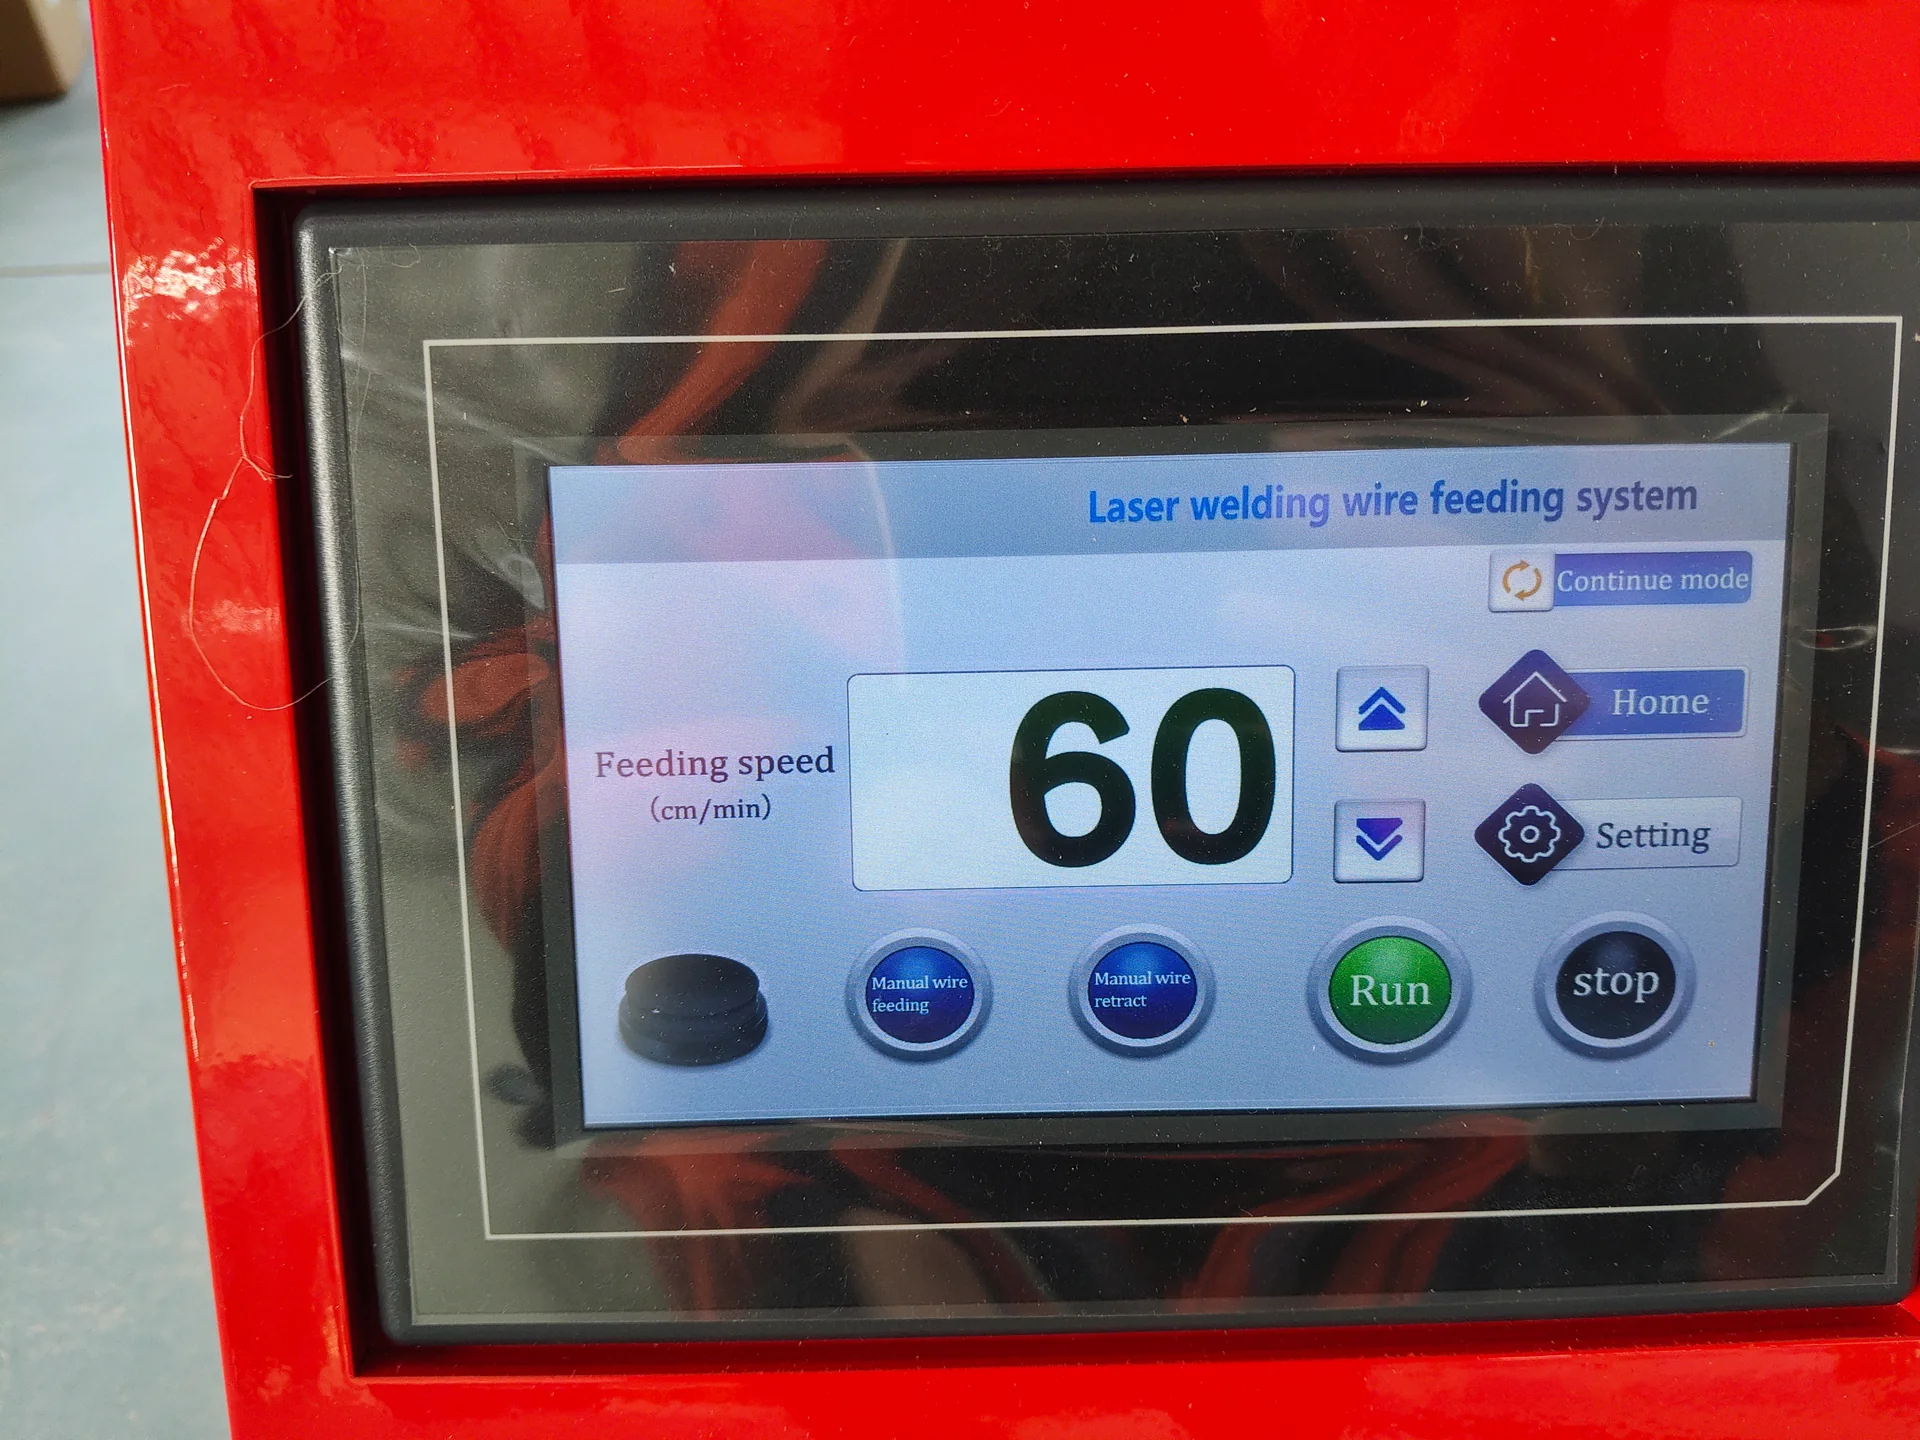
CHENDA supplies handheld laser welding equipment for steel, stainless steel and selected aluminium alloys. The range includes water-cooled configurations and external wire feeders with touchscreen control, plus automatic and robotic laser welding systems.
Explore CHENDA Handheld Laser Welders.
11. Questions to Ask Before Buying
- What thickness can the unit weld single-side and both sides in my material?
- Which laser source brand and power?
- Air or water cooling, and what duty cycle?
- Is a wire feeder included, and which wire sizes?
- Is wobble included, and what width?
- Which safety items come with the machine, and what must I provide?
- What are the consumables and their prices?
- Can you weld my sample part before I order?
Frequently Asked Questions
Is handheld laser welding faster than TIG?
On suitable seams, yes: a manufacturer reports up to 4× faster welding than TIG and MIG. Total job time falls less — about 30% in the example above — unless finishing also drops.
How thick can a 1,500 W handheld laser weld?
About 4 mm single-side in stainless steel, mild steel and aluminium, about 1 mm in copper, and up to about 10 mm welded from both sides.
How thick can a 1,000 W or 2,000 W handheld laser weld?
Vendor guides put 1,000 W at about 3 mm of steel and 2,000 W at up to about 8 mm. Test your own joint.
How much does a handheld laser welder cost?
Chinese listings run about US$1,600–7,900 for 1,000–3,000 W machines. Add a laser-safe area, eyewear and fume extraction.
Is laser welding stronger than MIG?
Not inherently. Strength depends on the joint design, fusion and penetration. MIG is better for large structural fillets.
Can handheld laser welding handle gaps?
Small gaps, with wire feed and wobble. Large or variable gaps are better suited to MIG.
Is handheld laser welding safe in an open workshop?
No. Class 4 handheld lasers need a controlled area, laser-rated eyewear and trained operators.
Request a Handheld Laser Welding Recommendation
Send us:
- Material grade and thickness
- A joint drawing or photo
- Required weld quality and monthly volume
- Country and current welding process
Explore CHENDA Handheld Laser Welders · Request a Technical Equipment Quote
Email: info@chendalaser.com · Phone: +86 153 0644 7102